
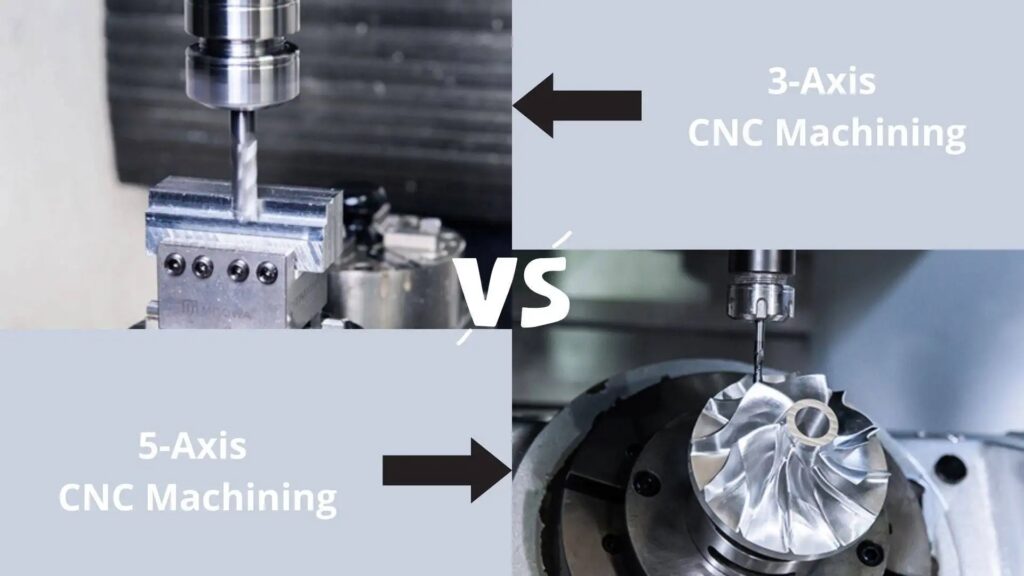
For product designers and procurement managers, choosing the correct milling configuration is a critical decision that impacts part cost, dimensional accuracy, and lead times. Balancing design intent with budgets requires understanding 3-Axis vs 5-axis CNC milling, especially how multi-axis setups perform compared with standard machining methods.
Before diving into technical specifics, let us establish the fundamental differences:
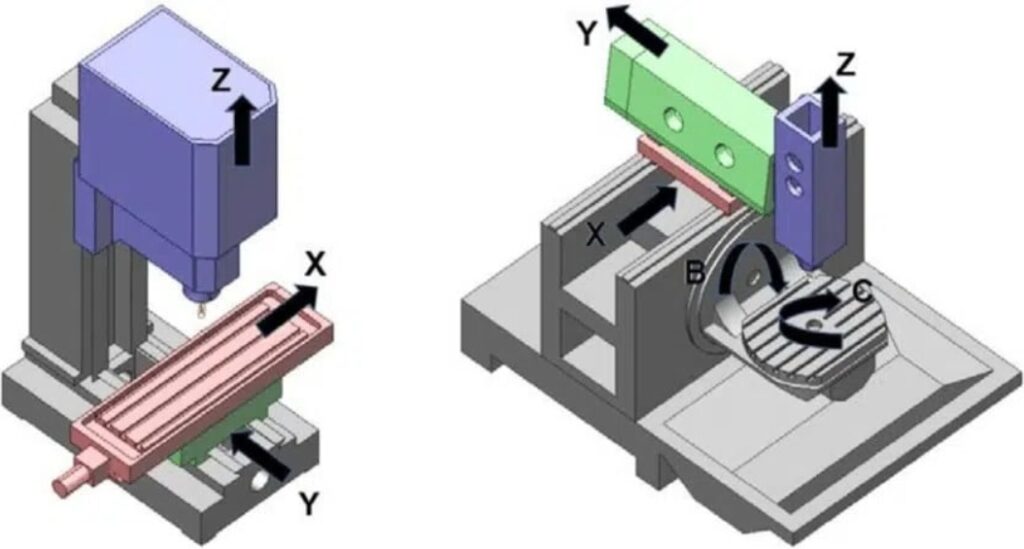
l Kinematic Versatility: Standard 3-Axis CNC machining moves along linear Cartesian coordinates, whereas 5-Axis CNC machining adds rotational axes for complex, multi-angle cutting.
l Precision Integrity: Repetitive CNC re-fixturing on 3-axis setups introduces cumulative CNC tolerance stack-up, while single setup CNC machining on a 5-axis system can finish complex geometries from multiple directions with fewer datum changes.
l Procurement Optimization: Understanding when to use 5-Axis CNC machining is frequently an economic decision. The ability to reduce CNC setups and manual intervention can offset the higher machine-hour cost of multi-axis equipment.
l Strategic Partnership: Aligning with an experienced partner like Rejin CNC, an aluminum CNC machining supplier and aluminum CNC machining manufacturer China, helps product teams use DFM analysis to select the most cost-effective machining path.
Kinematic differences between 3-axis vs. 5-axis CNC milling configurations control toolpath options, fixture needs, part access, and machine build limits.
Standard 3-axis CNC machining still serves as the main choice in factories. It brings simple operation, lower setup costs, and solid output for flat or box-like shapes.
These machines follow a basic setup.
l Three-Axis Linear Movement: The cutting tool travels along the usual X, Y, and Z lines. The part stays fixed in its clamp.
l Setup Complexity and Re-fixturing: Work on a multi-sided part calls for turning it by hand and CNC re-fixturing each new side. This takes extra time and may build up CNC tolerance stack-up on key spots.
l Geometrical Limitations and Tool Reach: The tool stays in one angle. So undercuts, slanted faces, or hidden spots often call for special fixtures or more setups.
For basic housings, plates, brackets, and parts like these, 3-Axis CNC machining stays quick and cost-effective.
Advanced 5-Axis CNC machining builds on straight linear moves by adding two turning axes. These let the tool or part tilt and rotate during the cut.
This setup brings extra flexibility and better tool control:
l Rotational Axis Integration: The two extra turning axes improve 5-Axis tool access. Cutters can reach complex surfaces from many angles.
l Simultaneous 5-Axis Machining: In simultaneous 5-Axis machining, the linear and turning axes work together without pause. This suits sculpted surfaces, turbine-style contours, impellers, and other complex organic shapes.
l 3+2-Axis Machining: 3+2-Axis machining turns the rotational axes to set a fixed angle and then locks the part in place. Standard three-axis cutting follows. The method provides solid rigidity for multi-face and angled features without needing full five-axis moves all the time.
Understanding when to use 5-Axis CNC machining over standard setups depends primarily on geometry, tolerance relationships, tool access, setup count, and production economics.
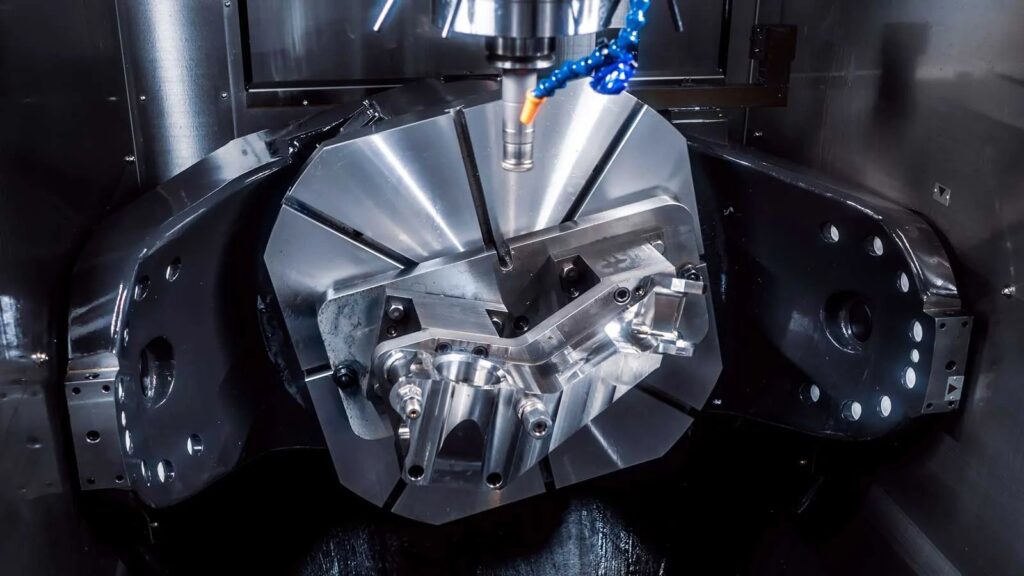
When manufacturing high-precision components, manual repositioning between machining operations can become a major source of dimensional deviation.
Eliminating unnecessary intervention protects tight dimensions:
l Eliminating Re-Fixturing Errors: Single setup CNC machining allows multiple faces and features to be machined relative to one primary datum, reducing alignment shifts caused by repeated CNC re-fixturing.
l Unified Datum Alignment: Fewer setups help control CNC tolerance stack-up across holes, bores, mating faces, and other geometrically related features.
When positional relationships across several faces are more important than individual feature tolerances, this is often a strong reason for deciding when to use 5-Axis CNC machining.
Modern structural components frequently contain angled holes, internal cavities, tight fillets, and deep recesses that are difficult to reach using conventional vertical mills.
These tool movements improve cutter interaction:
l 5-Axis Tool Access: Better 5-Axis tool access allows shorter and stiffer cutting tools to reach angled or recessed areas, helping reduce tool deflection and vibration.
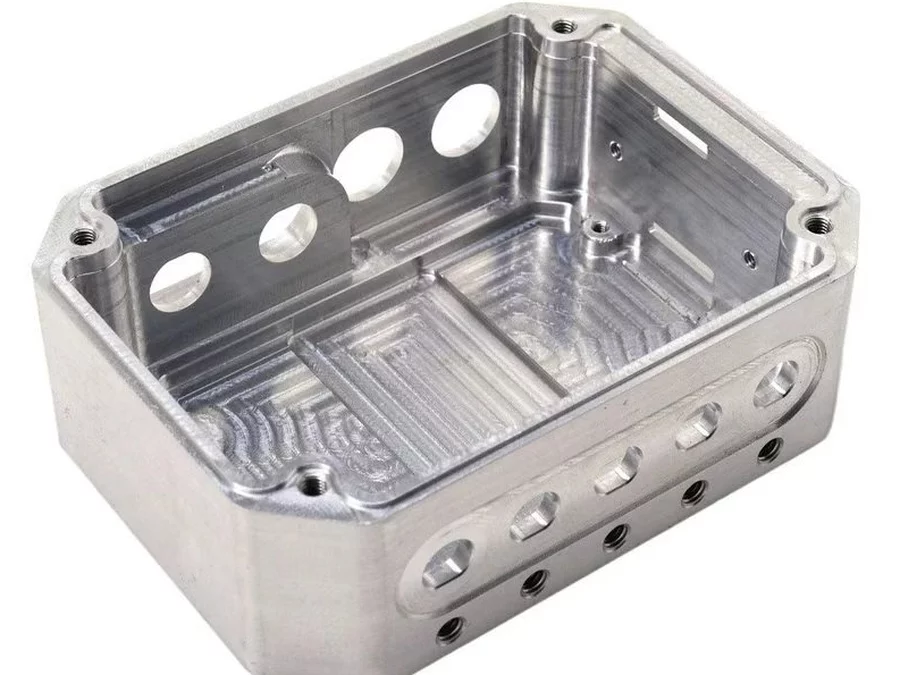
l Deep Pocket CNC Machining: During deep pocket CNC machining, tilting the tool or workpiece can improve tool clearance and reduce dependence on long, unstable cutters.
This advantage is particularly important for aluminum housings, aerospace structures, robotics components, and other parts requiring complex multi-sided CNC machining.
Machining four, five, or more faces creates a throughput bottleneck on conventional systems.
Consolidating operations onto one machining center improves efficiency:
l Reducing Work-Holding Setups: Multi-sided CNC machining on a 5-axis center can combine several operations into one clamping, helping reduce CNC setups, fixture changes, and operator intervention.
l Optimized Tooling and Cycle Times: Eliminating repeated alignment and CNC re-fixturing can reduce non-cutting time even when the hourly rate of 5-Axis CNC machining is higher.
For many procurement projects, the ability to reduce CNC setups is just as important as machining complex geometry.
B2B buyers have to weigh technical performance against unit costs, production volume, fixture expenses, inspection needs, and programming investment.
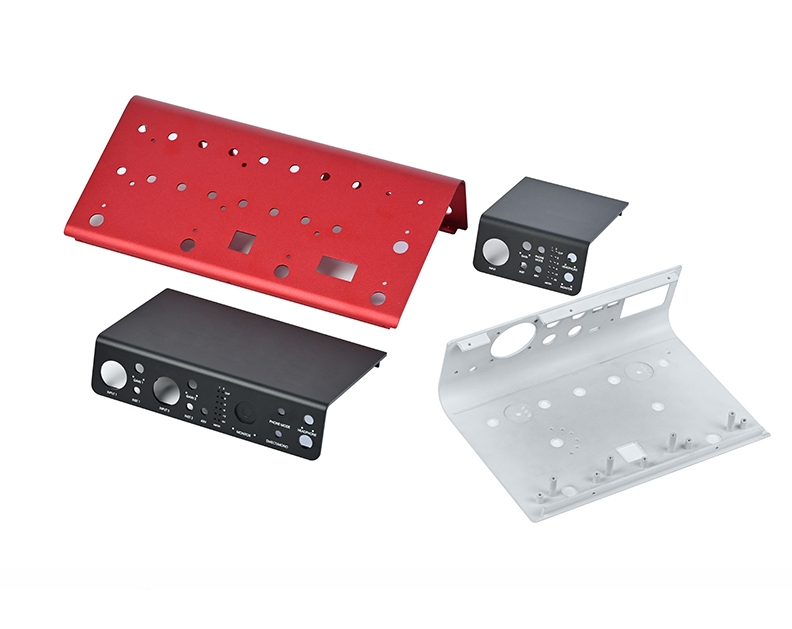
A realistic 3-Axis vs 5-Axis machining cost comparison looks at total manufacturing cost. It does not focus on the machine-hour rate alone.
These cost drivers change with part complexity and production volume:
l Programming and Initial Setup Costs: 5-Axis CNC machining needs more advanced CAM programming and machine setup. This creates higher upfront engineering costs than standard 3-Axis CNC machining.
l Part Quantity and Complexity Thresholds: When a part requires repeated CNC re-fixturing, custom fixtures, and multiple inspections, the 3-Axis vs 5-Axis machining cost gap can narrow. A 5-axis process may combine several operations.
l Stamping vs. CNC Machining Choice: High-volume simple parts may move to stamping or other tooling-based processes. Complex enclosures and precision structural parts can stay suitable for multi-sided CNC machining.
Procurement teams should calculate 3-Axis vs 5-Axis machining cost by looking at programming, fixture fabrication, setup labor, machine time, inspection, scrap risk, and production volume together.
Practical production illustrates how selecting the right machining configuration affects quality and efficiency.
Case studies demonstrate the benefits of choosing the appropriate setup:
l Automotive Fluid Connector Assembly: For pressure-rated fluid connectors, single setup CNC machining can help maintain concentricity and alignment between critical features.
l Premium Audio Enclosure Case Study: Cosmetic aluminum enclosures with multiple machined faces can benefit from 5-Axis CNC machining when reducing fixture changes improves both dimensional consistency and surface quality.
l Robotics Joint Component Application: Multi-axis robotic joint brackets requiring accurate relationships between bores, mating faces, and angled features are strong candidates for multi-sided CNC machining in a single setup.
For aluminum applications, working with an experienced aluminum CNC machining supplier can help determine whether 3+2-Axis machining, simultaneous 5-Axis machining, or conventional 3-axis milling offers the best balance.
Choosing between 3-Axis vs 5-Axis CNC milling depends on finding the point where geometry, tolerance, production volume, setup time, and unit cost align.
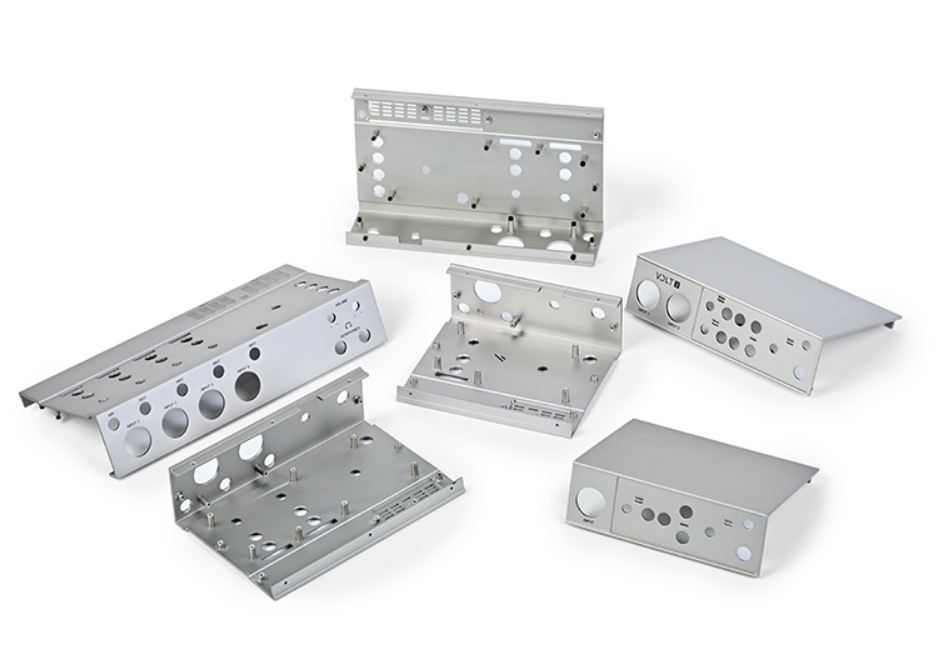
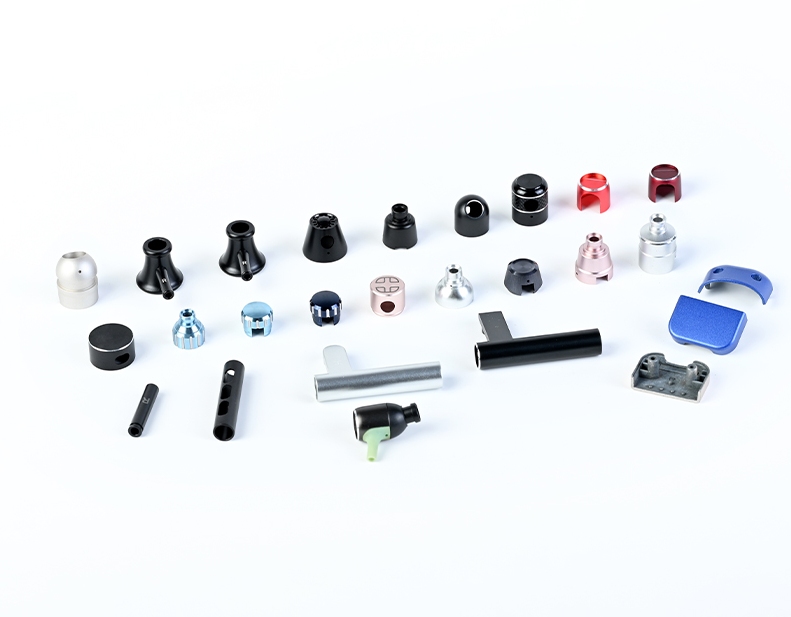
At Rejin CNC, we specialize in bridging the gap between complex designs and scalable manufacturing. As a capable 5-Axis CNC machining manufacturer, aluminum CNC machining supplier, and aluminum CNC machining manufacturer China, Rejin CNC supports prototype and production projects requiring 3-Axis CNC machining, 3+2-Axis machining, simultaneous 5-Axis machining, and single setup CNC machining.
Our engineering team provides DFM support to help evaluate when to use 5-Axis CNC machining, improve 5-Axis tool access, control CNC tolerance stack-up, and reduce CNC setups before production begins.
Contact Rejin CNC to submit your CAD drawings and request a machining review and quotation.
A: Use 3+2-Axis machining for prismatic parts with flat or angled faces that can be indexed into position. Simultaneous 5-Axis machining is more appropriate for complex curved surfaces requiring continuous changes in tool orientation.
A: Align features with common machining directions, standardize tool access, simplify deep pockets, and reduce unnecessary side features. Good DFM can reduce CNC setups even when 3-Axis CNC machining is retained.
A: Single setup CNC machining reduces repeated CNC re-fixturing, helping maintain a common datum across multiple faces and minimizing CNC tolerance stack-up.
A: Consider 5-Axis CNC machining when the part requires extensive multi-sided CNC machining, difficult 5-Axis tool access, deep pocket CNC machining, tight cross-face positional tolerances, or enough setup consolidation to justify the higher machine cost.
A: No. Although 5-axis equipment has a higher hourly rate, 3-Axis vs 5-Axis machining cost depends on total setup labor, fixture requirements, programming, inspection, cycle time, and scrap risk. Parts requiring many separate setups may be more economical on a 5-axis machine.
Your message lands directly with our senior engineers — instantly acknowledged.
We study your requirements and propose a workable solution with material & process options.
Detailed quotation with specs, options and lead time — no hidden fees.
Approve the sample, then we mass-produce with full QC and on-time shipping.
WhatsApp: +86 13790500374
Email: info@rejincnc.com
Your CAD files are kept strictly confidential. Quotation within 24 hours.