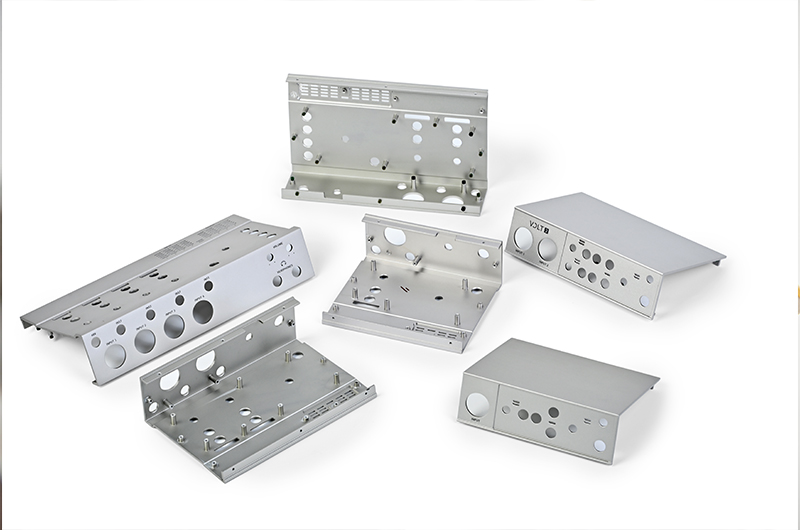
cnc machining case studies、precision parts case studies

Backed by ISO9001 & IATF16949 full-process quality control, we assign seasoned project managers to tackle all your OEM project challenges and technical difficulties.
We advance sustainable green CNC manufacturing, and deliver customized precision metal parts to global leading enterprises with reliable end-to-end support.
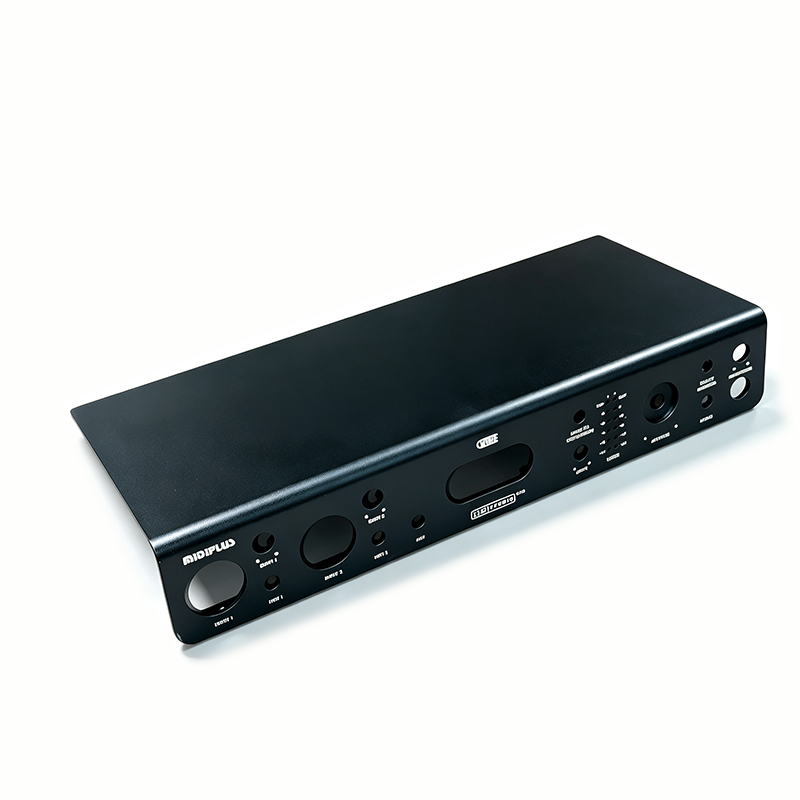
Audio Control Panel

Custom CNC Machined Aluminum Audio Control Panel for Premium Audio Brands

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important}body .produc-banner{display:none!important}.rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px}.rjc-wrap *{box-sizing:border-box}.rjc-wrap img{max-width:100%;height:auto}.rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600}.rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5}.rjc-wrap h2{font-size:32px;margin:0 0 8px}.rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px}.rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto}.rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/Audio-Control-Panel.jpg') center 30%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)}.rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2}.rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none}.rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none}.rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)}.rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px}.rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px}.rjc-hero-left{max-width:780px}.rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3}.rjc-viz-b1{top:14%;right:6%}.rjc-viz-b2{bottom:20%;right:6%}.rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px}.rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase}.rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px}.rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)}.rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85}.rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px}.rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px}.rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px}.rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1}.rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)}.rjc-cta:hover::after{transform:translateX(4px)}.rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px}.rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1}.rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)}.rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px}.rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none}.rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none}.rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1}.rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1}.rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1}.rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1}.rjc-sec{margin-bottom:48px}.rjc-sec-head{text-align:center;margin-bottom:32px}.rjc-sec-head .rjc-sub{margin-top:6px}.rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center}.rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)}.rjc-list{margin:16px 0 0;padding:0;list-style:none}.rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px}.rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px}.rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px}.rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease}.rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)}.rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px}.rjc-card h3{font-size:18px;margin:0 0 8px}.rjc-card p{font-size:14px;margin:0;color:#6b6f7a}.rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px}.rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7}.rjc-story strong{color:#1C2333}.rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0}.rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start}.rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center}.rjc-pain h3{font-size:16px;margin:0 0 4px}.rjc-pain p{font-size:14px;margin:0;color:#6b6f7a}.rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px}.rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px}.rjc-sol h3{font-size:16px;margin:0 0 6px}.rjc-sol p{font-size:14px;margin:0;color:#6b6f7a}.rjc-challs{display:grid;gap:18px}.rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px}.rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px}.rjc-chall h3{font-size:18px;margin:0}.rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px}.rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c}.rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px}.rjc-ch-line b.pr{color:#D64545}.rjc-ch-line b.fx{color:#4376FB}.rjc-ch-line b.rs{color:#2E9E5B}.rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB}.rjc-diff-item h3{font-size:16px;margin:0 0 6px}.rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a}.rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px}.rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep}.rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7}.rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1}.rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px}.rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px}.rjc-step p{font-size:14px;margin:0;color:#6b6f7a}.rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)}.rjc-table{width:100%;border-collapse:collapse;font-size:14.5px}.rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase}.rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c}.rjc-table tr:nth-child(even) td{background:#FAFBFF}.rjc-table td:first-child{font-weight:500;color:#1C2333}.rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff}.rjc-results h2{color:#fff}.rjc-results .rjc-sub{color:#aeb6cc}.rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px}.rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center}.rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600}.rjc-res b em{font-style:normal;color:#4376FB}.rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4}.rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px}.rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px}.rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333}.rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px}.rjc-media{border-radius:14px;overflow:hidden;box-shadow:0 12px 34px rgba(28,35,51,.16);background:#000;margin-top:22px}.rjc-media img{display:block;width:100%;height:auto;border-radius:14px}.rjc-cap{font-size:12.5px;color:#8a8f9c;text-align:center;margin:10px 0 0}.rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s}.rjc-btn:hover{background:#1C2333;color:#fff}.rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)}.rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff}@media (max-width:991px){.rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/Audio-Control-Panel.jpg') center/cover no-repeat}.rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px}.rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px}.rjc-2col{grid-template-columns:1fr;gap:24px}.rjc-cards,.rjc-steps{grid-template-columns:1fr}.rjc-res-grid{grid-template-columns:repeat(2,1fr)}.rjc-quotes{grid-template-columns:1fr}.rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr}.rjc-chall .rjc-ch-lines{grid-template-columns:1fr}}@media (max-width:575px){.rjc-stats{grid-template-columns:1fr 1fr;gap:10px}.rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px}.rjc-cta-sec{padding:36px 22px}} ±0.02 mmOne-Datum Cutout Tolerance 6063-T5Aluminum · In-House Anodized CNC Machining Case Study · Audio Equipment Premium Audio Front Panels Machined to ±0.02 mm Feature Alignment — From One 6063-T5 Billet A desktop amplifier brand was losing units to panels whose legends, jacks and knobs never lined up with the PCB. Rejin CNC machined every control surface, cutout and silk-print feature on a single 5-axis datum — held to ±0.02 mm, anodized in-house, and running 80,000+ pieces a year without a single re-work. See How We Solved ItGet a Free DFM Review ±0.02 mmCutout-to-legend positional tolerance, CMM verified 80k+Pieces per year, same panel shipped on time 6063-T5Extruded aluminum, one-billet machined, no weld seams IATF 16949In-house QC & full lot traceability The Story The Panel No Shop Could Get Right A premium desktop amplifier, a front face that had to be perfect, and the clamping strategy that finally made it so. The problem was never a single hole or a single finish. It was the relationship between them. The customer is a European audio brand building a compact desktop amplifier. The front panel is the product’s identity: brushed 6063 aluminum, laser-etched legends, recessed jacks, encoder knobs and a VFD window. Each feature had to meet the internal PCB, the faceplate overlay and the cabinet shell within a few hundredths of a millimeter. Over six months, several suppliers took a shot. Shop A held individual holes to spec but could not repeat the distance between them — a jack measured fine alone, but sat 0.3 mm off its legend after anodizing. Shop B proposed die-casting to save cost, which changed the weight, the look and the whole product. Shop C nailed the samples, then shipped mismatched legends and inconsistent brushing at 5,000 pieces a month. “The panel looks perfect on the bench. It only fails when someone plugs a cable in.” The brand’s sourcing engineer reached out to Rejin CNC. Our process engineer did not just quote the drawing — the DFM review flagged the datum-drift problem and proposed a fix no other shop had raised: machine the entire panel from one billet in one 5-axis setup, referenced to a single origin, so every cutout, engraving and silk-print feature shares the same coordinates before anodizing. The first article landed exactly where the PCB expected it. The customer’s assembly line stopped re-working panels. That golden sample has run 80,000+ pieces a year for three years. The finished panel — one 6063-T5 billet, one datum, every cutout and legend held to ±0.02 mm. “A panel that measures fine alone still fails if its features do not share the same origin. We machined it that way from the first chip.” Customer Pain Points Why Previous Suppliers Could Not Deliver Six problems every candidate shop failed to solve before Rejin CNC. 1 Feature-to-feature drift Individual holes were within spec, but the relationship between jacks, knobs and legends moved 0.2–0.3 mm — panels did not line up with the internal PCB. 2 Anodizing shifts the legend Color and texture variation after anodizing made laser-engraved legends look washed out or misregistered — two problems in one finish. 3 Brushing direction mismatch Brushed finish direction varied panel to panel. On a premium product sitting on a desk, that is the first thing a customer notices. 4 Thin-wall warping The panel is only 2.5 mm thick. Machining distortion made flatness drift past spec, causing the panel to rock on the cabinet. 5 No engineering feedback Suppliers quoted drawings as-is and called drift “normal for anodizing” — nobody proposed a better clamping or datum strategy. 6 Volume collapse Sample quality was fine, but at 5,000+ pieces per month, lead times slipped and batch consistency fell apart. Project Overview 6063-T5 Aluminum Audio Control Panels for a Global Pro-Audio Brand CNC-machined aluminum front panels for desktop amplifiers and audio interfaces — built around Rejin CNC’s one-datum clamping strategy: the entire panel is roughed, semi-finished and finished in a single 5-axis setup, with every cutout, engraving and silk-print feature referenced to one origin. 6063-T5 extruded aluminum, full panel machined from one billet — no weld seams, no assembled corners One-datum clamping on 5-axis integrated fixture — ±0.02 mm feature-to-feature positional tolerance Multi-texture finish: brushed, sandblasted and anodized in-house; laser-engraved legends registered to the same datum Recessed jacks, encoder bores and VFD window machined to mate directly with customer’s PCB and cabinet IATF 16949 process control, FAI on first article, CMM on critical features of every batch 5-axis one-setup machining — every feature shares the same datum, before anodizing. Our Engineering Solution How We Engineered the Panel for Repeatable Production The difference was never a single machine — it was a complete engineering system built around one datum. Clamping One-Datum Fixture Strategy A dedicated vacuum + mechanical fixture locates the billet from one corner. Roughing, semi-finishing and finishing never re-independently locate the part — datum-to-datum error is eliminated, not compensated. Machining 5-Axis One-Setup Program The entire panel is completed in a single 5-axis cycle. Thin walls are supported throughout; light finishing passes control deflection and heat, holding ±0.02 mm on critical features. Surface In-House Brushing & Anodizing Brushing direction is controlled by a dedicated fixture; anodizing runs under our own roof with titrated chemistry and colorimeter check against a master — no batch-to-batch drift. Marking Registered Laser Legends Legends are laser-engraved after anodizing, registered to the same datum used for cutouts. What the mill machined is exactly where the engraver marks it. Inspection CMM + Optical Registration Check Every batch gets CMM measurement of critical cutout positions and an optical check of legend registration — data archived per lot for full traceability. Engineering DFM-First Review We review the CAD before tooling, flag the features most sensitive to datum drift, and design the process around them. The review that won this customer is free on every project. Visual surface inspection — brushing direction, anodized color and legend legibility checked on every lot. Why one datum wins Most shops locate the part once per operation. Each re-clamp reintroduces datum error, and anodizing adds its own small movement. By machining to a single datum from rough to finish — and engraving legends to that same origin afterward — the relative positions of every feature stay locked, batch after batch. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the production floor — root cause, fix, and the result we hold today. 📐 Thin-Wall Panel Warping Problem2.5 mm thin panel warped during milling, causing flatness drift and rocking on the cabinet. FixVacuum + mechanical support fixture holds the billet throughout; low-stress toolpaths and separated rough/finish passes control heat and deflection. ResultFlatness held within 0.05 mm across the panel — no rocking, no re-work at the customer’s assembly line. 🎯 Legend Registration Drift ProblemLaser legends landed slightly off the jacks and knobs after anodizing — the exact flaw that failed previous suppliers. FixEngraving is programmed to the same datum used for CNC cutouts; optical registration check verifies every batch against the golden panel. ResultLegend-to-feature registration held within ±0.02 mm — no misprinted panels across 80,000+ pieces. 🎨 Anodizing Color & Brush Direction ProblemColor drifted between batches and brushing direction varied — unacceptable on a premium desktop product. FixIndependent in-house surface workshop: titrated bath chemistry, same-batch processing, colorimeter ΔE check against retained master, and a brushing-direction fixture. ResultUniform color and brush direction across months of production — panels from different batches are visually indistinguishable. 📈 Scaling to 80,000 Pieces / Year ProblemThe product line ramped to 80,000+ panels per year — most shops lose quality or lead time at that pace. FixDedicated machining cells, standardized fixtures, SPC on critical dimensions, and a fixed monthly shipping schedule agreed with the customer. Result100% batch consistency with on-time delivery — sustained for three straight years of production. Manufacturing Process From 6063 Billet to Finished Panel in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 Material & Traceability 6063-T5 extruded aluminum is selected with mill certificate; heat lot and traceability ID are recorded for every batch. 2 5-Axis One-Datum Machining Billet clamped on a dedicated fixture; rough, semi-finish and finish in one setup — every feature referenced to the same origin. 3 Brushing & Surface Prep Controlled brushing direction removes tool marks and prepares an even surface for anodizing. 4 Anodizing & Color Check In-house anodizing with colorimeter verification against the master sample — ΔE kept under 1.0 batch to batch. 5 Laser Legend Registration Legends are laser-engraved to the same datum as the cutouts — sharp, fade-resistant, and perfectly aligned. 6 CMM, Optical Check & Packing CMM on critical features, optical legend-registration check, and protective packing before export — defects never ship. In-house machining cell — 200+ 5/3-axis CNC machines, dedicated surface workshop, standardized QC. Why the first article is the golden sample Because every feature shares one datum, the first article that passes FAI becomes the reference for every batch that follows. We do not “tune” the process on the customer’s volume order — we lock it at sample stage, then hold it. Quality Assurance Measured Results, Not Promises Every key specification is verified with CMM, optical registration and colorimeter on every production batch — data archived per lot. Specification Customer Requirement Achieved Method Feature-to-feature tolerance ±0.05 mm ±0.02 mm CMM measurement Legend registration Aligned to cutouts Within ±0.02 mm Optical registration check Panel flatness ≤0.10 mm ≤0.05 mm Surface plate + dial gauge Anodizing color ΔE < 2.0 vs. master ΔE < 1.0 avg Colorimeter Surface finish (brushed) Uniform direction 100% consistent Visual inspection Batch consistency 100% critical-feature check 100% pass CMM + optical per lot Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The brand compared us against shops in three countries. Here is what closed the deal. vs. re-clamped setups One-datum machining strategy No datum loss between operations. Every feature is referenced to the same origin — the relative accuracy that re-clamped setups simply cannot match. vs. outsourced anodizing 200+ machines + in-house surface workshop Milling, brushing, anodizing and laser marking under one roof — no hand-offs, no color drift, no third-party excuses. vs. batch sampling IATF 16949 + 100% critical check Critical features measured on every batch, legends optically verified — defects never ship to your assembly line. vs. sales-led quoting Process engineers answer your CAD You talk directly to the engineers who run the process — DFM feedback in 48 hours, technical answers in hours, not days. Project Results What Three Years of Partnership Delivered The first batch fully met the brand’s standards, and the program has only grown since. ±0.02 mmFeature-to-feature tolerance held at volume, CMM verified 80k+Panels per year, on-time for three straight years 0Mis-registered legends found at customer assembly ΔE < 1.0Anodized color consistency batch to batch Customer Feedback What the OEM Buyers Say Direct quotes from the people who run this program on the customer side. “The legends finally line up with the jacks and knobs. We stopped re-working panels on our assembly line — something previous suppliers could not fix.” Product EngineerEuropean Pro-Audio Brand “Batch after batch, the anodizing color and brushing direction match the golden sample. We stopped checking surface finish on arrival.” Quality ManagerAudio Equipment OEM “Rejin’s DFM flagged the datum-drift issue our previous suppliers never mentioned. Delivery has been on time at 80,000+ pieces a year for three years.” Sourcing LeadGlobal Audio Brand Free DFM Check · Quote in 24 Hours Have a Similar CNC Audio Panel or Enclosure Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
Custom CNC Machined Audio Enclosures with Embedded Seamless Riveting

Custom CNC Machined Audio Enclosures with Embedded Seamless Riveting

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important}body .produc-banner{display:none!important}.rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px}.rjc-wrap *{box-sizing:border-box}.rjc-wrap img{max-width:100%;height:auto}.rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600}.rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5}.rjc-wrap h2{font-size:32px;margin:0 0 8px}.rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px}.rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto}.rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/Custom-CNC-Machined-Audio-Enclosures-with-Embedded-Seamless-Riveting.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)}.rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2}.rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none}.rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none}.rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)}.rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px}.rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px}.rjc-hero-left{max-width:780px}.rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3}.rjc-viz-b1{top:14%;right:6%}.rjc-viz-b2{bottom:20%;right:6%}.rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px}.rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase}.rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px}.rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)}.rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85}.rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px}.rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px}.rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px}.rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1}.rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)}.rjc-cta:hover::after{transform:translateX(4px)}.rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px}.rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1}.rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)}.rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px}.rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none}.rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none}.rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1}.rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1}.rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1}.rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1}.rjc-sec{margin-bottom:48px}.rjc-sec-head{text-align:center;margin-bottom:32px}.rjc-sec-head .rjc-sub{margin-top:6px}.rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center}.rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)}.rjc-list{margin:16px 0 0;padding:0;list-style:none}.rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px}.rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px}.rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px}.rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease}.rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)}.rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px}.rjc-card h3{font-size:18px;margin:0 0 8px}.rjc-card p{font-size:14px;margin:0;color:#6b6f7a}.rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px}.rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7}.rjc-story strong{color:#1C2333}.rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0}.rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start}.rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center}.rjc-pain h3{font-size:16px;margin:0 0 4px}.rjc-pain p{font-size:14px;margin:0;color:#6b6f7a}.rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px}.rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px}.rjc-sol h3{font-size:16px;margin:0 0 6px}.rjc-sol p{font-size:14px;margin:0;color:#6b6f7a}.rjc-challs{display:grid;gap:18px}.rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px}.rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px}.rjc-chall h3{font-size:18px;margin:0}.rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px}.rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c}.rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px}.rjc-ch-line b.pr{color:#D64545}.rjc-ch-line b.fx{color:#4376FB}.rjc-ch-line b.rs{color:#2E9E5B}.rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB}.rjc-diff-item h3{font-size:16px;margin:0 0 6px}.rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a}.rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px}.rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep}.rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7}.rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1}.rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px}.rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px}.rjc-step p{font-size:14px;margin:0;color:#6b6f7a}.rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)}.rjc-table{width:100%;border-collapse:collapse;font-size:14.5px}.rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase}.rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c}.rjc-table tr:nth-child(even) td{background:#FAFBFF}.rjc-table td:first-child{font-weight:500;color:#1C2333}.rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff}.rjc-results h2{color:#fff}.rjc-results .rjc-sub{color:#aeb6cc}.rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px}.rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center}.rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600}.rjc-res b em{font-style:normal;color:#4376FB}.rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4}.rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px}.rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px}.rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333}.rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px}.rjc-media{border-radius:14px;overflow:hidden;box-shadow:0 12px 34px rgba(28,35,51,.16);background:#000;margin-top:22px}.rjc-media img{display:block;width:100%;height:auto;border-radius:14px}.rjc-cap{font-size:12.5px;color:#8a8f9c;text-align:center;margin:10px 0 0}.rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s}.rjc-btn:hover{background:#1C2333;color:#fff}.rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)}.rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff}@media (max-width:991px){.rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/Custom-CNC-Machined-Audio-Enclosures-with-Embedded-Seamless-Riveting.jpg') center/cover no-repeat}.rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px}.rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px}.rjc-2col{grid-template-columns:1fr;gap:24px}.rjc-cards,.rjc-steps{grid-template-columns:1fr}.rjc-res-grid{grid-template-columns:repeat(2,1fr)}.rjc-quotes{grid-template-columns:1fr}.rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr}.rjc-chall .rjc-ch-lines{grid-template-columns:1fr}}@media (max-width:575px){.rjc-stats{grid-template-columns:1fr 1fr;gap:10px}.rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px}.rjc-cta-sec{padding:36px 22px}} Embedded RivetingSelf-Developed Process IATF 16949Certified Production CNC Machining Case Study · Audio Equipment CNC Audio Enclosures with Embedded Seamless Riveting — Zero Backplate Rivet Marks A European audio brand spent months rejecting enclosures with visible rivet marks on the backplate. Rejin CNC’s self-developed embedded seamless riveting delivers a fully flat back with zero through-holes — machined to ±0.01 mm, anodized in-house, and IATF 16949 verified at volume. See How We Solved ItGet a Free DFM Review 0Rivet marks on backplate — fully flat surface ±0.01 mmDimensional tolerance, CMM verified 200+Amada 3/5-axis CNC machines in-house IATF 16949Certified production & quality control The Story How This Project Really Began A real engineering story — a visible flaw, three failed suppliers, and the process that fixed it. Some of the best engineering stories start with a tiny visible flaw. For a European audio brand preparing to launch a new analog amp simulator, the flaw sat right on the backplate: rows of raised rivet marks that made a premium product look cheap. The product was a compact guitar amp simulator — designed in France, sold worldwide. The industrial design was clean: a brushed aluminum housing with laser-marked control graphics, engineered for the tone-focused musicians who would buy it. On the front, the product looked flawless. On the back, traditional through riveting left raised dents where rivets penetrated the aluminum plate. Every unit carried the marks, and every unit undermined the premium look the brand had spent years building. For months, the brand’s sourcing team searched for a better answer. They evaluated machine shops in three countries. Some shops said the marks were unavoidable — “that’s just how riveting works.” Others offered to hide the marks with stickers or paint, which the engineers rejected outright. One supplier quoted a cheaper die-cast alternative that changed the product’s weight, feel and cost. None of them solved the real problem. Then the brand’s team was referred to Rejin CNC. Instead of quoting the drawing as-is, our engineers ran a free DFM review and proposed something the other shops had never mentioned: an embedded seamless riveting process — nut columns pressed inward from the back, sealed inside the material, with zero through-holes and a completely flat backplate. No marks. No dents. No stickers. “The backplate is the face nobody talks about — until it ruins the product.” How the first sample changed everything. The first article arrived with a backplate so flat that the customer’s quality team ran their fingers across it twice to confirm. Dimension checks passed on the first pass. Assembly fit was perfect. The embedded rivet structure passed pull-out testing with margins to spare. That first article became the reference baseline for every batch that followed — and the brand never looked back. The Customer’s Pain Points Why Previous Suppliers Could Not Deliver Six problems that every candidate shop failed to solve before Rejin CNC. 1 Visible rivet marks Through rivets left raised dents on the backplate — every single unit carried the marks that broke the clean surface. 2 Cheap premium look The dents made a high-end audio product look low-cost on retail shelves, directly hurting the brand’s positioning. 3 Weak joint confidence Rivets penetrating the plate compromised structural integrity and risked clearance issues with internal electronics. 4 Anodizing inconsistency Color drifted between batches, and marks became even more visible after coating — two problems in one finish. 5 No engineering feedback Suppliers quoted drawings as-is and called rivet marks “unavoidable” instead of proposing a better process. 6 Unreliable scale-up Shops handled samples but lost quality or deadlines when production ramped to volume. Project Overview Audio Equipment Enclosures with Seamless Backplates for Global Audio Brands CNC-machined aluminum housings for audio equipment — amp simulators, sound cards and audio interfaces — built around Rejin CNC’s self-developed embedded seamless riveting: a fully flat backplate with zero rivet marks, one-piece structure and optimized strength. 6063-T5 extruded aluminum, precision CNC machined with 5-axis integrated clamping Embedded seamless riveting — one-piece connection, zero through-holes Matte/bright anodizing with laser-engraved logos, uniform finish ±0.01 mm dimensional tolerance, CMM verified on every batch IATF 16949 quality system, from prototype to mass production Traditional through riveting vs. our embedded seamless process — appearance and strength both optimized. Our Engineering Solution How We Engineered the Part for Repeatable Production The difference was never a single machine — it was a complete engineering system built around one process. Riveting Embedded Seamless Riveting Nut columns are pressed inward and sealed inside the material in a single operation — no through-holes, no raised marks, and a fully flat backplate that passes the fingertip test every time. Machining 5-Axis One-Piece Clamping Billet machining with 5-axis integrated clamping holds thin-wall geometry without distortion, keeping tolerance within ±0.01 mm on critical features. Surface In-House Sandblasting & Anodizing Matte or bright anodizing with laser-engraved logos runs under our own roof — uniform surface finish, no third-party hand-offs, no color drift. Inspection Full Dimension CMM Every critical feature is CMM-measured on every part, with data archived per production lot for full traceability. Quality IATF 16949 Process Control Standardized inspection and SPC keep batch consistency high — the same quality that automotive OEMs require, applied to audio hardware. Engineering DFM-First Approach We review your CAD before tooling, flag manufacturability issues, and design the process around the part — the review that won this customer is free for every project. Cutaway view — nut columns embedded inward, no through-hole, zero backplate marks. Why embedded riveting wins Standard riveting pushes rivets through the plate, leaving dents on the back and compromising internal component clearance. Our embedded process seats the nut column inside the material — the back stays smooth, the joint stays strong, and the product finally looks the way it should. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the production floor — root cause, fix, and the result we hold today. 🧱 Thin-Wall Distortion in Machining ProblemThin-wall sections warped during CNC machining, causing uneven gaps at assembly and inconsistent tolerance across parts. Fix5-axis integrated clamping holds the billet in one piece; low-stress toolpaths and separated rough/finish passes control heat and deflection. Result±0.01 mm tolerance held at volume — every part measures inside spec, batch after batch. 🔩 Rivet Pull-Down Marks on the Backplate ProblemStandard riveting pulled material and left visible dents — the exact flaw that failed three previous suppliers. FixSelf-developed embedded rivet die with controlled press force seats the nut column inward, sealing it inside the material with zero surface disturbance. ResultZero rivet marks on the backplate — fully flat surface confirmed by visual and surface-gauge inspection on every batch. 🎨 Anodizing Color Drift ProblemAnodizing color drifted between batches, and surface flaws became more visible after coating. FixIndependent in-house surface workshop with titrated bath chemistry, same-batch processing and colorimeter verification against a retained master sample. ResultUniform color across batches and years — parts from different months are visually indistinguishable. 🚚 Scaling Prototype to Mass Production ProblemThe launch plan demanded a sharp volume increase — most shops lose quality or lead time at that pace. FixDedicated machining cells, standardized fixtures, SPC on critical dimensions and a fixed shipping schedule agreed with the customer. Result100% batch consistency with on-time delivery — sustained for three straight years of production. Manufacturing Process From Aluminum Billet to Finished Enclosure in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 Aluminum Billet & Extrusion 6063-T5 aluminum billet is selected and extruded to near-net shape — stable material properties and lower machining stock for every run. 2 5-Axis CNC Machining Billet machining with 5-axis integrated clamping holds thin-wall geometry — tolerance controlled within ±0.01 mm on critical features. 3 Embedded Seamless Riveting Self-developed riveting joins the housing in a single process — nut columns embedded inward, zero through-holes, fully flat backplate. 4 Sandblasting Uniform matte surface prep removes machining traces and prepares the part for an even coating. 5 Anodizing & Laser Marking Matte or bright anodizing with laser-engraved logos — consistent color, sharp and fade-resistant graphics. 6 Full Inspection & Packing Full dimension CMM inspection, batch consistency check and protective packing before export — defects never ship. From aluminum billet to finished product — 200+ Amada 3/5-axis CNC machines, independent surface workshop, standardized QC. Embedded riveting hardware Our engineers developed this process in-house. The nut column is pressed inward and sealed inside the material — watch how the backplate stays perfectly flat with zero marks. Quality Assurance Measured Results, Not Promises Every key specification is verified with CMM, surface gauge and colorimeter on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Backplate flatness Fully flat, zero rivet marks 100% pass Visual + surface gauge Machining tolerance ±0.01 mm ±0.01 mm CMM measurement Rivet joint strength Meets OEM pull-out spec Passed Pull-out test Anodizing color ΔE < 1.5 vs. master ΔE < 1.0 avg Colorimeter Salt spray resistance 72 h, no corrosion Passed ASTM B117 Batch consistency 100% dimension inspection 100% pass Full dimension CMM Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The brand compared us against shops in three countries. Here is what closed the deal. vs. standard riveting Self-developed embedded riveting Zero through-holes, flat backplate, stronger joint — a process customers cannot get from commodity shops, protected by years of in-house refinement. vs. outsourced finishing 200+ machines + in-house surface workshop Machining, sandblasting, anodizing and laser marking under one roof — no hand-offs, no color drift, no third-party excuses. vs. batch sampling IATF 16949 + 100% inspection Critical dimensions measured on every part, every batch verified — defects never ship to your line. vs. sales-led support Engineers answer your questions You talk directly to the people who run the machines and the process — technical answers in hours, DFM in 48. Project Results What Three Years of Partnership Delivered The first batch fully met the brand’s standards, and the relationship has only grown since. 0Rivet marks on backplate — fully flat surface 100%Batch consistency, every lot verified ±0.01 mmHeld at volume, CMM verified 3+Years of stable mass production Customer Feedback What the OEM Buyers Say Direct quotes from the people who run this program on the customer side. “The backplate is finally completely smooth. No rivet marks, no dents — it looks the way a premium product should.” Product ManagerEuropean Audio Brand “Batch after batch, the anodizing color matches the reference sample. We stopped checking color on arrival.” Quality ManagerAudio Equipment OEM “Rejin’s DFM caught assembly issues our previous suppliers never mentioned. Delivery has been on time for three straight years.” Sourcing LeadGlobal Audio Brand Free DFM Check · Quote in 24 Hours Have a Similar CNC Enclosure or Audio Part Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
Extruded 6063 Aluminum Audio Enclosure

Custom CNC Machined Audio Enclosure Case Study

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important} body .produc-banner{display:none!important} .rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px} .rjc-wrap *{box-sizing:border-box} .rjc-wrap img{max-width:100%;height:auto} .rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600} .rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5} .rjc-wrap h2{font-size:32px;margin:0 0 8px} .rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px} .rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto} .rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)} .rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2} .rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none} .rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none} .rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)} .rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px} .rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px} .rjc-hero-left{max-width:780px} .rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3} .rjc-viz-b1{top:14%;right:6%} .rjc-viz-b2{bottom:20%;right:6%} .rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px} .rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase} .rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px} .rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)} .rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85} .rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px} .rjc-stat{background:rgba(255,255,255,.08);border:1px solid rgba(255,255,255,.14);border-radius:12px;padding:18px 16px} .rjc-stat b{display:block;font-size:24px;color:#fff;font-weight:600;letter-spacing:.5px} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.4;display:block;margin-top:4px} .rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px} .rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px} .rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1} .rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)} .rjc-cta:hover::after{transform:translateX(4px)} .rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px} .rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1} .rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)} .rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px} .rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none} .rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none} .rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1} .rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1} .rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1} .rjc-sec{margin-bottom:48px} .rjc-sec-head{text-align:center;margin-bottom:32px} .rjc-sec-head .rjc-sub{margin-top:6px} .rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center} .rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)} .rjc-list{margin:16px 0 0;padding:0;list-style:none} .rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px} .rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px} .rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px} .rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease} .rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)} .rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px} .rjc-card h3{font-size:18px;margin:0 0 8px} .rjc-card p{font-size:14px;margin:0;color:#6b6f7a} .rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px} .rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7} .rjc-story strong{color:#1C2333} .rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0} .rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start} .rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center} .rjc-pain h3{font-size:16px;margin:0 0 4px} .rjc-pain p{font-size:14px;margin:0;color:#6b6f7a} .rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px} .rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px} .rjc-sol h3{font-size:16px;margin:0 0 6px} .rjc-sol p{font-size:14px;margin:0;color:#6b6f7a} .rjc-challs{display:grid;gap:18px} .rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px} .rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px} .rjc-chall h3{font-size:18px;margin:0} .rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px} .rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c} .rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px} .rjc-ch-line b.pr{color:#D64545} .rjc-ch-line b.fx{color:#4376FB} .rjc-ch-line b.rs{color:#2E9E5B} .rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB} .rjc-diff-item h3{font-size:16px;margin:0 0 6px} .rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a} .rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px} .rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep} .rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7} .rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1} .rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px} .rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px} .rjc-step p{font-size:14px;margin:0;color:#6b6f7a} .rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)} .rjc-table{width:100%;border-collapse:collapse;font-size:14.5px} .rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase} .rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c} .rjc-table tr:nth-child(even) td{background:#FAFBFF} .rjc-table td:first-child{font-weight:500;color:#1C2333} .rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff} .rjc-results h2{color:#fff} .rjc-results .rjc-sub{color:#aeb6cc} .rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px} .rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center} .rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600} .rjc-res b em{font-style:normal;color:#4376FB} .rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4} .rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px} .rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px} .rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333} .rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px} .rjc-cta{background:linear-gradient(135deg,#4376FB,#2f5be8);border-radius:16px;padding:48px 44px;text-align:center;color:#fff} .rjc-cta h2{color:#fff;font-size:28px;margin:0 0 10px} .rjc-cta p{color:#dbe4ff;margin:0 auto 26px;max-width:620px;font-size:15px} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap} .rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s} .rjc-btn:hover{background:#1C2333;color:#fff} .rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)} .rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff} @media (max-width: 991px){ .rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center/cover no-repeat} .rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px} .rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px} .rjc-stats{grid-template-columns:repeat(2,1fr)} .rjc-2col{grid-template-columns:1fr;gap:24px} .rjc-cards,.rjc-steps{grid-template-columns:1fr} .rjc-res-grid{grid-template-columns:repeat(2,1fr)} .rjc-quotes{grid-template-columns:1fr} .rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr} .rjc-chall .rjc-ch-lines{grid-template-columns:1fr} } @media (max-width: 575px){ .rjc-stats{grid-template-columns:1fr 1fr;gap:10px} .rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px} .rjc-cta{padding:36px 22px} } /* ===== v10.14 hover-fix 临时内联:ghost 按钮 hover 白底变蓝字 ===== */ .rjc-btn.rjc-btn-ghost:hover{color:#4376FB!important} .rjc-btn:hover{color:#fff!important} ±0.01 mmCMM Verified IATF 16949Certified Production CNC Machining Case Study · Premium Audio Custom CNC Machined Audio Enclosures — Held to ±0.01 mm, On Time Every Time A premium European audio brand spent eight months and twelve failed suppliers hunting for enclosures that held tolerance at volume. Rejin CNC machined their thin-wall 6063-T5 aluminum enclosure to ±0.01 mm — brushed, black-anodized and CMM-verified — then shipped 20,000+ units a month on schedule for three straight years. See How We Solved ItGet a Free DFM Review 6063-T5Aluminum alloy, extruded + precision CNC machined ±0.01 mmTolerance held at volume, CMM verified 20,000+Enclosures per month, prototype to mass production 100%On-time delivery, 3 years running The Story How This Project Really Began A real engineering story — the search, the failures, and the first DFM call that changed everything. Every difficult CNC project starts with a problem nobody else wants to solve. This one started in Germany, where a premium audio brand was preparing to launch a new generation of control units. The industrial design was stunning: a slim, minimalist enclosure in brushed, black-anodized aluminum. The engineering team loved it. The manufacturing team did not. The enclosure was compact, with wall sections as thin as 1.2 mm, visible surfaces that demanded a perfectly horizontal brushed texture, and a black anodized finish that had to stay color-stable across tens of thousands of parts. On paper, it looked like a routine CNC job. In reality, it was a test that most machine shops quietly failed. For eight months, the brand’s sourcing team searched. They evaluated machine shops in three countries, ordered sample parts from more than a dozen candidates. Some delivered accurate dimensions but rough, blotchy surfaces. Some produced a beautiful first article — and then could never repeat it at volume. One factory quoted an attractive price, quietly outsourced the anodizing to a third party, and the color drifted from batch to batch. Another could only run short runs of 500 parts, with no capacity to scale. Samples were good. Production was not. That is the classic gap in custom CNC machining, and it was costing the brand its entire launch calendar. “Send us your drawing, and we will tell you what is wrong with it before you spend a single dollar on tooling.” How Rejin CNC entered the picture. The brand’s sourcing team was referred to Rejin CNC by an industry contact. Instead of quoting the drawing as-is — the way every previous supplier had done — our engineers ran a free DFM review and came back with three pages of findings: two sharp internal corners that would create stress risers and risk cracking during anodizing, an undersized thread depth on the mounting boss, and a suggested wall-thickness adjustment that would cut distortion risk in half without changing the design language. The review took 48 hours. It was delivered before any purchase order existed. That single DFM review is what turned the conversation into a first sample order. The first article passed every single check on the customer’s list — dimension, surface, color, assembly fit. It did not just meet the standard; it set the baseline that every batch since has been measured against. The Customer’s Pain Points Why Previous Suppliers Could Not Deliver Six problems, repeated across more than a dozen candidate shops. 1 Anodizing color drift Black anodized batches drifted by ΔE > 3.0 against the master sample — unacceptable on a premium retail product where every unit must match. 2 Inconsistent brushed texture Brushing direction and depth varied from part to part and even within the same batch, ruining the “one continuous grain” look the design required. 3 Thin-wall distortion 1.2 mm wall sections warped during machining, leaving uneven gaps at assembly and forcing costly manual rework. 4 No scale-up capability Shops that handled 500-piece prototypes could not hold quality at 5,000, let alone 20,000+ units per month. 5 Unreliable lead times Missed ship dates and last-minute excuses forced the brand to keep unsafe inventory buffers and risk its retail calendar. 6 No engineering feedback Drawings were quoted as-is. Design issues surfaced only after tooling was cut and money was already spent. Project Overview Compact Control-Unit Enclosure for a European High-End Audio Brand A compact control-unit enclosure for a European high-end audio brand — engineered for precision fit, a horizontal brushed texture and color-stable black anodizing, produced from a single supplier with machining, finishing, laser marking and QC all in-house. 6063-T5 extruded aluminum + CNC machining, wall thickness down to 1.2 mm Horizontal brushed finish with color-stable black anodizing (ΔE < 1.5) Laser-marked panels with sharp, fade-resistant graphics Scaled from first article to 20,000+ units / month under SPC control 100% inspection on critical dimensions, every batch color-verified Our Engineering Solution How We Engineered the Part for Repeatable Production The difference was never a single machine — it was a complete engineering system built around one part. Material 6063-T5 Extruded Aluminum Extrusion gave us a near-net inner cavity and stable material properties run after run — lower machining stock, lower cost, and far better anodizing response than die-cast blanks other shops had proposed. Fixtures Zero-Distortion Clamping Custom vacuum fixtures and precision soft jaws hold every part identically without squeezing the 1.2 mm walls — the foundation of repeatable ±0.01 mm tolerance. Process Rough / Finish Separation Roughing removes stock and releases internal stress; parts settle; then finishing passes hold final geometry. Toolpaths are optimized for constant chip load and minimal tool deflection. Surface Controlled Brushing & Anodizing Dedicated brushing fixtures fix feed direction and pressure; anodizing bath chemistry is titrated per tank and color is verified against a retained master sample every batch. Inspection 100% Critical-Dimension CMM Key mounting and assembly features are measured on a CMM for every part in every batch — not sampled, not eyeballed — with data archived per production lot. Capacity Dedicated Cell, Planned Schedules A dedicated machining cell and fixed monthly production windows protect this program’s lead time, so the brand can commit dates to its retail calendar with confidence. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the production floor — root cause, fix, and the result we hold today. 🧱 Thin-Wall Distortion at 1.2 mm ProblemEarly samples warped 0.08–0.15 mm after machining — the clamp pressure and cutting heat deformed walls thinner than a credit card. FixRedesigned fixtures to vacuum-hold from the flat reference face, split roughing from finishing, added a settling period between the two, and dropped finishing feed rates to cut heat input. ResultFlatness held at 0.03 mm average — inside the customer’s 0.05 mm requirement — and assembly gaps became uniform across all batches. 🎯 One Continuous Brushed Grain ProblemHand-fed brushing left visible direction changes and depth differences between parts — the “one continuous grain” look broke across a batch of 500. FixBuilt dedicated brushing fixtures with a fixed feed path and constant pressure, and added a light-angle visual check to every inspection station. ResultBrushed texture consistency now passes 100% of visual + light-angle checks, and the customer has approved the standard as its reference for other projects. 🎨 Color-Stable Black Anodizing ProblemBlack anodizing drifted between batches — different dye uptake and tank age changed the black from warm to blue-ish, up to ΔE > 3.0. FixTitrated bath chemistry before every run, standardized rack loading and current density, and verified each batch against a retained master sample with a colorimeter. ResultBatch color now averages ΔE < 1.0 vs. master — well inside the ΔE < 1.5 requirement — and parts from different months are visually indistinguishable. 🚚 Scaling from Prototype to 20,000+ Units / Month ProblemThe customer’s launch plan demanded a 10× volume increase in one quarter — most shops lose control of quality or lead time at that pace. FixDedicated machining cell, parallel finishing and anodizing lines, SPC on critical dimensions, and a fixed weekly shipping schedule agreed with the customer. Result20,000+ units per month delivered with 100% on-time shipment and zero appearance-related complaints over three years of continuous production. Manufacturing Process From Drawing to Finished Enclosure in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 DFM & Fixture Design Engineers reviewed the CAD, optimized wall thickness and machining stock, then designed custom vacuum fixtures to hold every part identically — the foundation of repeatable tolerance. 2 CNC Machining 3-axis and 4-axis CNC milling centers rough and finish in separated operations, holding ±0.01 mm on critical features with constant chip-load toolpaths. 3 Deburring & Prep Automated and manual deburring removes edge marks, then parts are cleaned and prepped so the brushed texture comes out flawless. 4 Brushing & Black Anodizing Horizontal brushing gives the signature grain; sulfuric anodizing in a titrated bath produces a color-stable black, verified against the master sample. 5 Laser Marking Logos, model numbers and regulatory marks are laser-marked with fixture-located precision for sharp, fade-resistant graphics. 6 100% Inspection & Packing Every part is CMM-checked on critical dimensions, color-verified and individually wrapped to prevent scratches before export packaging. Quality Assurance Measured Results, Not Promises Every key specification is verified with CMM, profilometer and color measurement on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Machining tolerance ±0.01 mm ±0.01 mm CMM measurement Surface flatness 0.05 mm max 0.03 mm avg Height gauge / granite plate Anodizing color (black) ΔE < 1.5 vs. master ΔE < 1.0 avg Colorimeter Brushed texture Consistent grain direction 100% pass Visual + light-angle inspection Salt spray resistance 72 h, no corrosion Passed ASTM B117 Laser mark durability No fade after use Passed Abrasion / solvent test Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The brand compared us against shops in three countries. Here is what closed the deal. vs. quote-as-is shops DFM before the order We review the drawing and flag manufacturability issues before you spend on tooling — the review that first won this customer is free and standard for every project. vs. outsourced finishing Finishing 100% in-house Brushing, anodizing and laser marking run under our own roof — no hand-offs, no color drift, no third-party excuses between machining and the finished part. vs. batch sampling 100% inspection, not AQL sampling Critical dimensions are CMM-measured on every part and color is verified every batch, so a defect never ships to your line. vs. sales-led support Engineers answer your questions You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks. Project Results What Three Years of Partnership Delivered The first batch fully met the brand’s retail standards, and the relationship has only grown since. 0Appearance-related complaints from end users 100%On-time monthly deliveries, zero delays +20%Customer repurchase rate after metal upgrade 3Years of continuous production partnership Customer Feedback What the OEM Buyers Say Direct quotes from the people who run this program on the customer side. “We spent eight months looking for a partner who could hold both tolerance and surface finish at volume. Rejin’s first article passed everything — we stopped looking that day.” Purchasing DirectorEuropean Electronics Brand “The brushed texture and black anodizing are identical to our reference sample even after three years of production. Color has never been a discussion point on a single batch.” Quality ManagerEuropean Audio Brand “The metal material has an outstanding tactile feel. Customer repurchase rates increased by 20%, making them a key partner in our product upgrades.” Product ManagerNorth American Audio Equipment Supplier Free DFM Check · Quote in 24 Hours Have a Similar CNC Enclosure or Audio Part Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
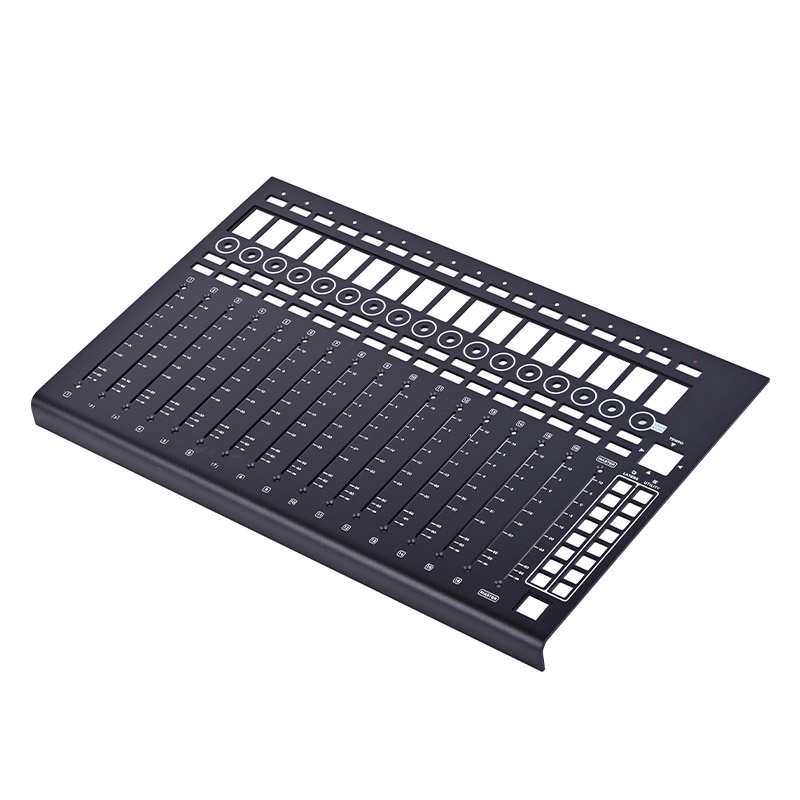
Products
Contacts
WhatsApp
Email