
CNC Machining Case Study · Audio Equipment
A European audio brand spent months rejecting enclosures with visible rivet marks on the backplate. Rejin CNC’s self-developed embedded seamless riveting delivers a fully flat back with zero through-holes — machined to ±0.01 mm, anodized in-house, and IATF 16949 verified at volume.
The Story
A real engineering story — a visible flaw, three failed suppliers, and the process that fixed it.
Some of the best engineering stories start with a tiny visible flaw. For a European audio brand preparing to launch a new analog amp simulator, the flaw sat right on the backplate: rows of raised rivet marks that made a premium product look cheap.
The product was a compact guitar amp simulator — designed in France, sold worldwide. The industrial design was clean: a brushed aluminum housing with laser-marked control graphics, engineered for the tone-focused musicians who would buy it. On the front, the product looked flawless. On the back, traditional through riveting left raised dents where rivets penetrated the aluminum plate. Every unit carried the marks, and every unit undermined the premium look the brand had spent years building.
For months, the brand’s sourcing team searched for a better answer. They evaluated machine shops in three countries. Some shops said the marks were unavoidable — “that’s just how riveting works.” Others offered to hide the marks with stickers or paint, which the engineers rejected outright. One supplier quoted a cheaper die-cast alternative that changed the product’s weight, feel and cost. None of them solved the real problem.
Then the brand’s team was referred to Rejin CNC. Instead of quoting the drawing as-is, our engineers ran a free DFM review and proposed something the other shops had never mentioned: an embedded seamless riveting process — nut columns pressed inward from the back, sealed inside the material, with zero through-holes and a completely flat backplate. No marks. No dents. No stickers.
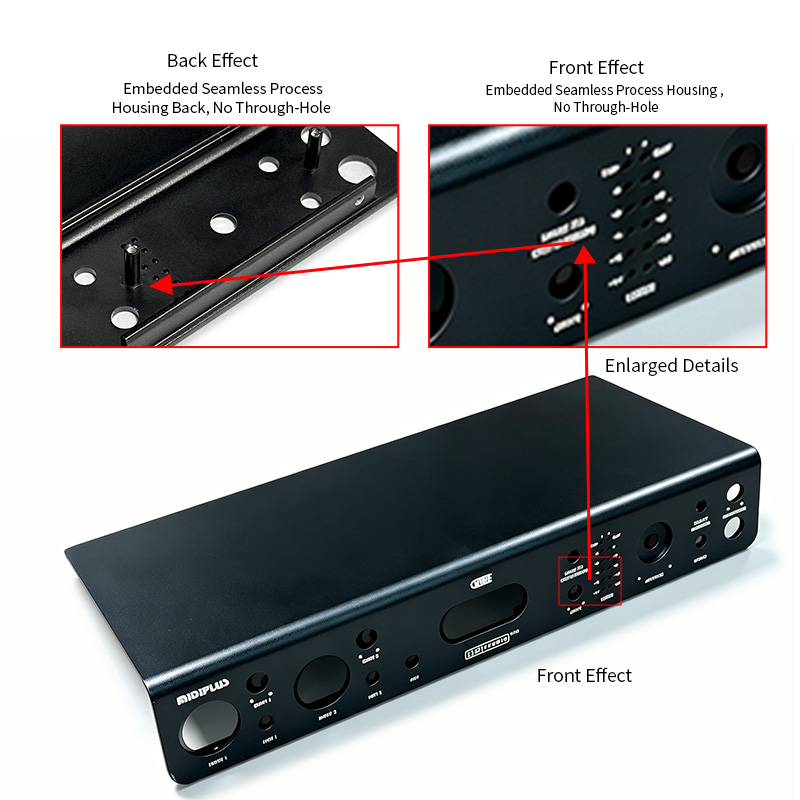
How the first sample changed everything. The first article arrived with a backplate so flat that the customer’s quality team ran their fingers across it twice to confirm. Dimension checks passed on the first pass. Assembly fit was perfect. The embedded rivet structure passed pull-out testing with margins to spare. That first article became the reference baseline for every batch that followed — and the brand never looked back.
The Customer’s Pain Points
Six problems that every candidate shop failed to solve before Rejin CNC.
Through rivets left raised dents on the backplate — every single unit carried the marks that broke the clean surface.
The dents made a high-end audio product look low-cost on retail shelves, directly hurting the brand’s positioning.
Rivets penetrating the plate compromised structural integrity and risked clearance issues with internal electronics.
Color drifted between batches, and marks became even more visible after coating — two problems in one finish.
Suppliers quoted drawings as-is and called rivet marks “unavoidable” instead of proposing a better process.
Shops handled samples but lost quality or deadlines when production ramped to volume.
Project Overview
CNC-machined aluminum housings for audio equipment — amp simulators, sound cards and audio interfaces — built around Rejin CNC’s self-developed embedded seamless riveting: a fully flat backplate with zero rivet marks, one-piece structure and optimized strength.
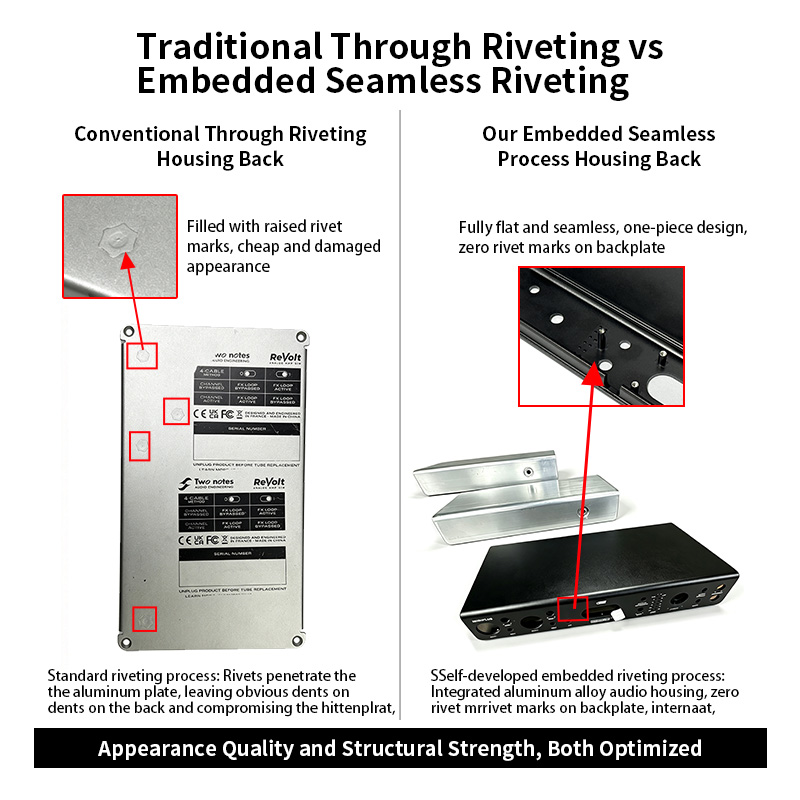
Traditional through riveting vs. our embedded seamless process — appearance and strength both optimized.
Our Engineering Solution
The difference was never a single machine — it was a complete engineering system built around one process.
Riveting
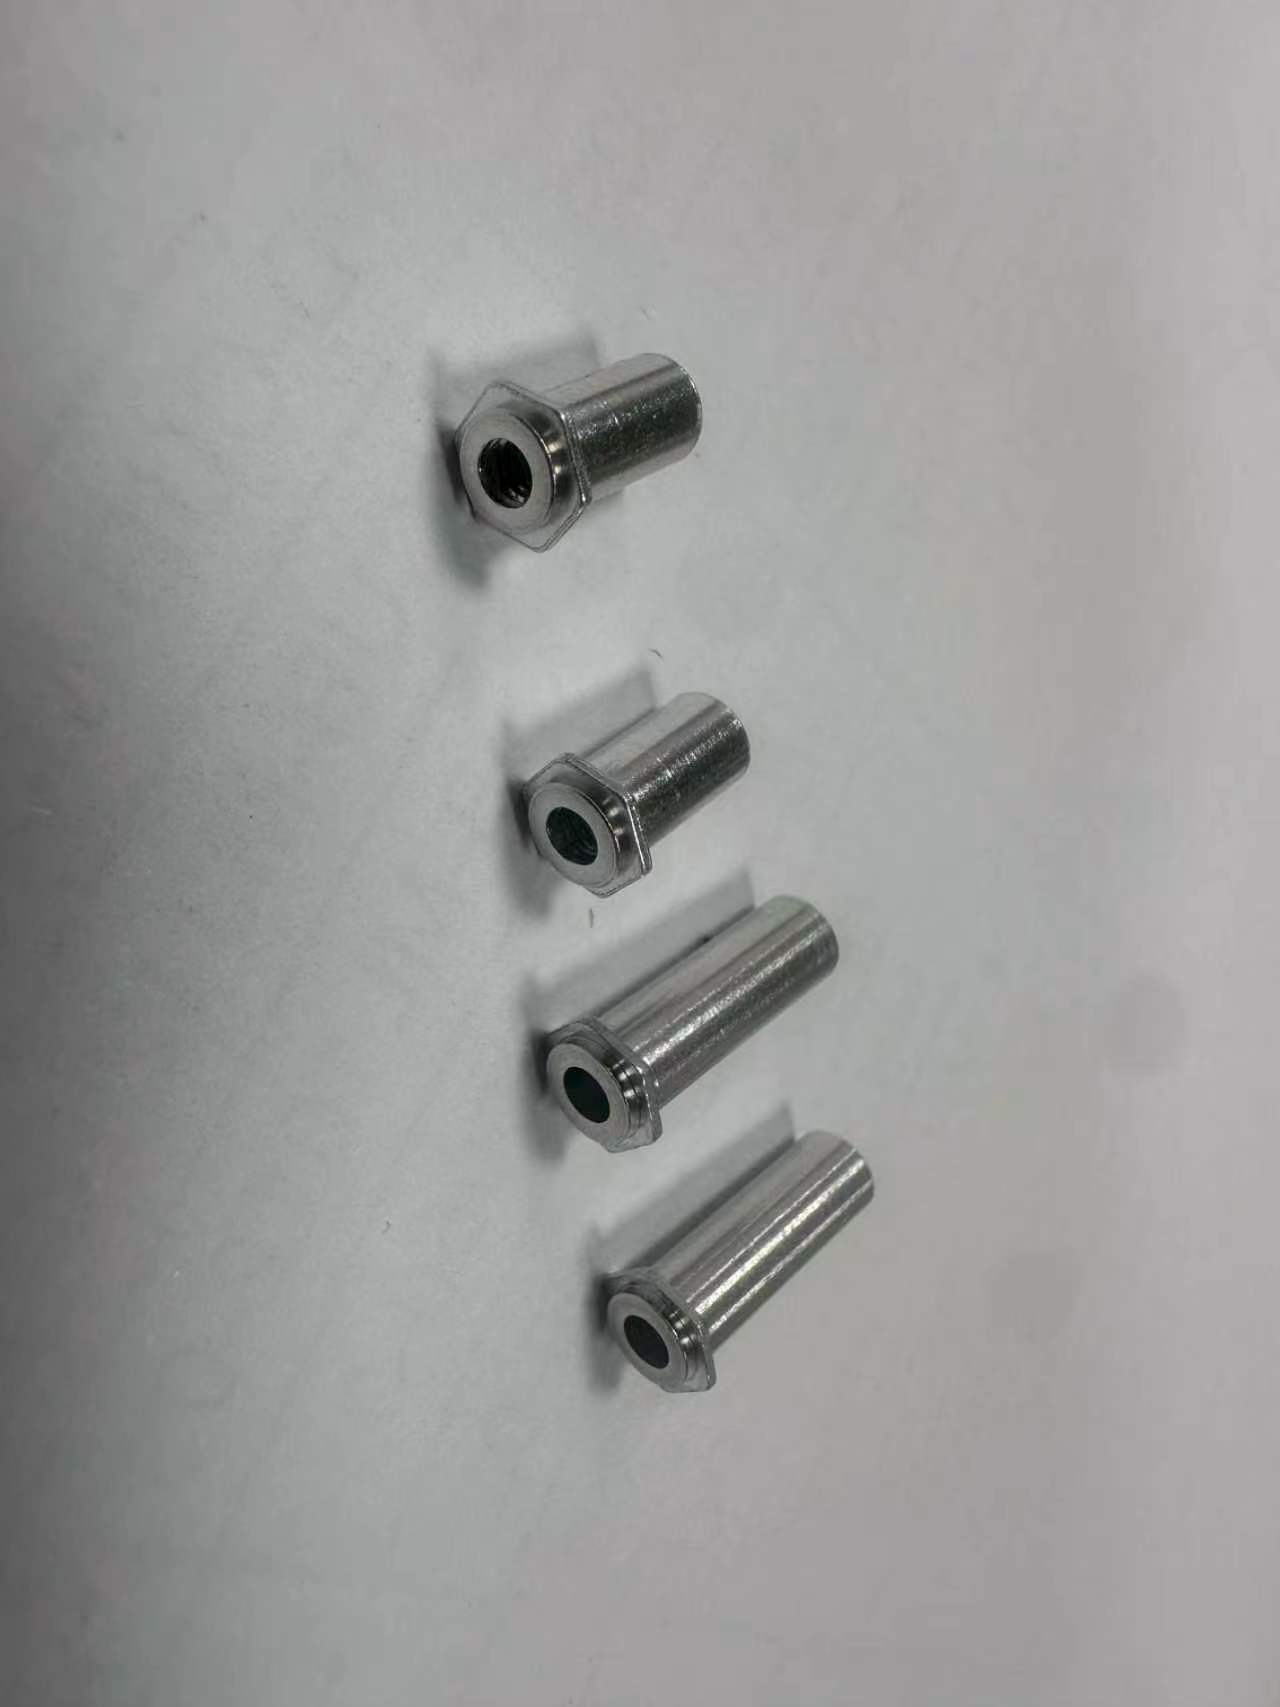
Nut columns are pressed inward and sealed inside the material in a single operation — no through-holes, no raised marks, and a fully flat backplate that passes the fingertip test every time.
Machining
Billet machining with 5-axis integrated clamping holds thin-wall geometry without distortion, keeping tolerance within ±0.01 mm on critical features.
Surface
Matte or bright anodizing with laser-engraved logos runs under our own roof — uniform surface finish, no third-party hand-offs, no color drift.
Inspection
Every critical feature is CMM-measured on every part, with data archived per production lot for full traceability.
Quality
Standardized inspection and SPC keep batch consistency high — the same quality that automotive OEMs require, applied to audio hardware.
Engineering
We review your CAD before tooling, flag manufacturability issues, and design the process around the part — the review that won this customer is free for every project.
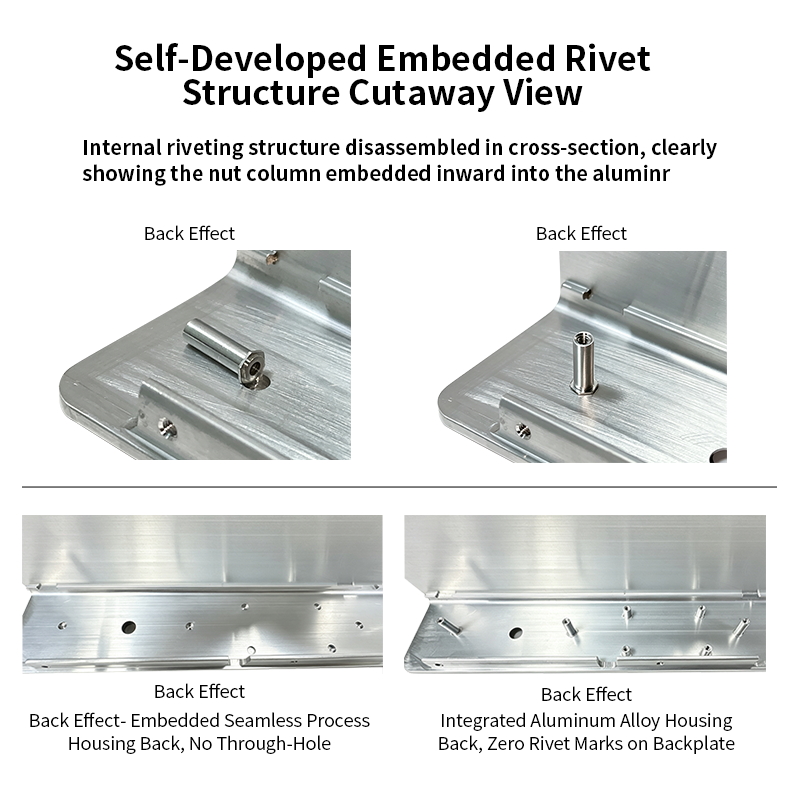
Cutaway view — nut columns embedded inward, no through-hole, zero backplate marks.
Standard riveting pushes rivets through the plate, leaving dents on the back and compromising internal component clearance. Our embedded process seats the nut column inside the material — the back stays smooth, the joint stays strong, and the product finally looks the way it should.
Challenges We Overcame
Real problems from the production floor — root cause, fix, and the result we hold today.
Manufacturing Process
Every step is documented with in-process inspection, so quality is built in — not inspected in at the end.
6063-T5 aluminum billet is selected and extruded to near-net shape — stable material properties and lower machining stock for every run.
Billet machining with 5-axis integrated clamping holds thin-wall geometry — tolerance controlled within ±0.01 mm on critical features.
Self-developed riveting joins the housing in a single process — nut columns embedded inward, zero through-holes, fully flat backplate.
Uniform matte surface prep removes machining traces and prepares the part for an even coating.
Matte or bright anodizing with laser-engraved logos — consistent color, sharp and fade-resistant graphics.
Full dimension CMM inspection, batch consistency check and protective packing before export — defects never ship.
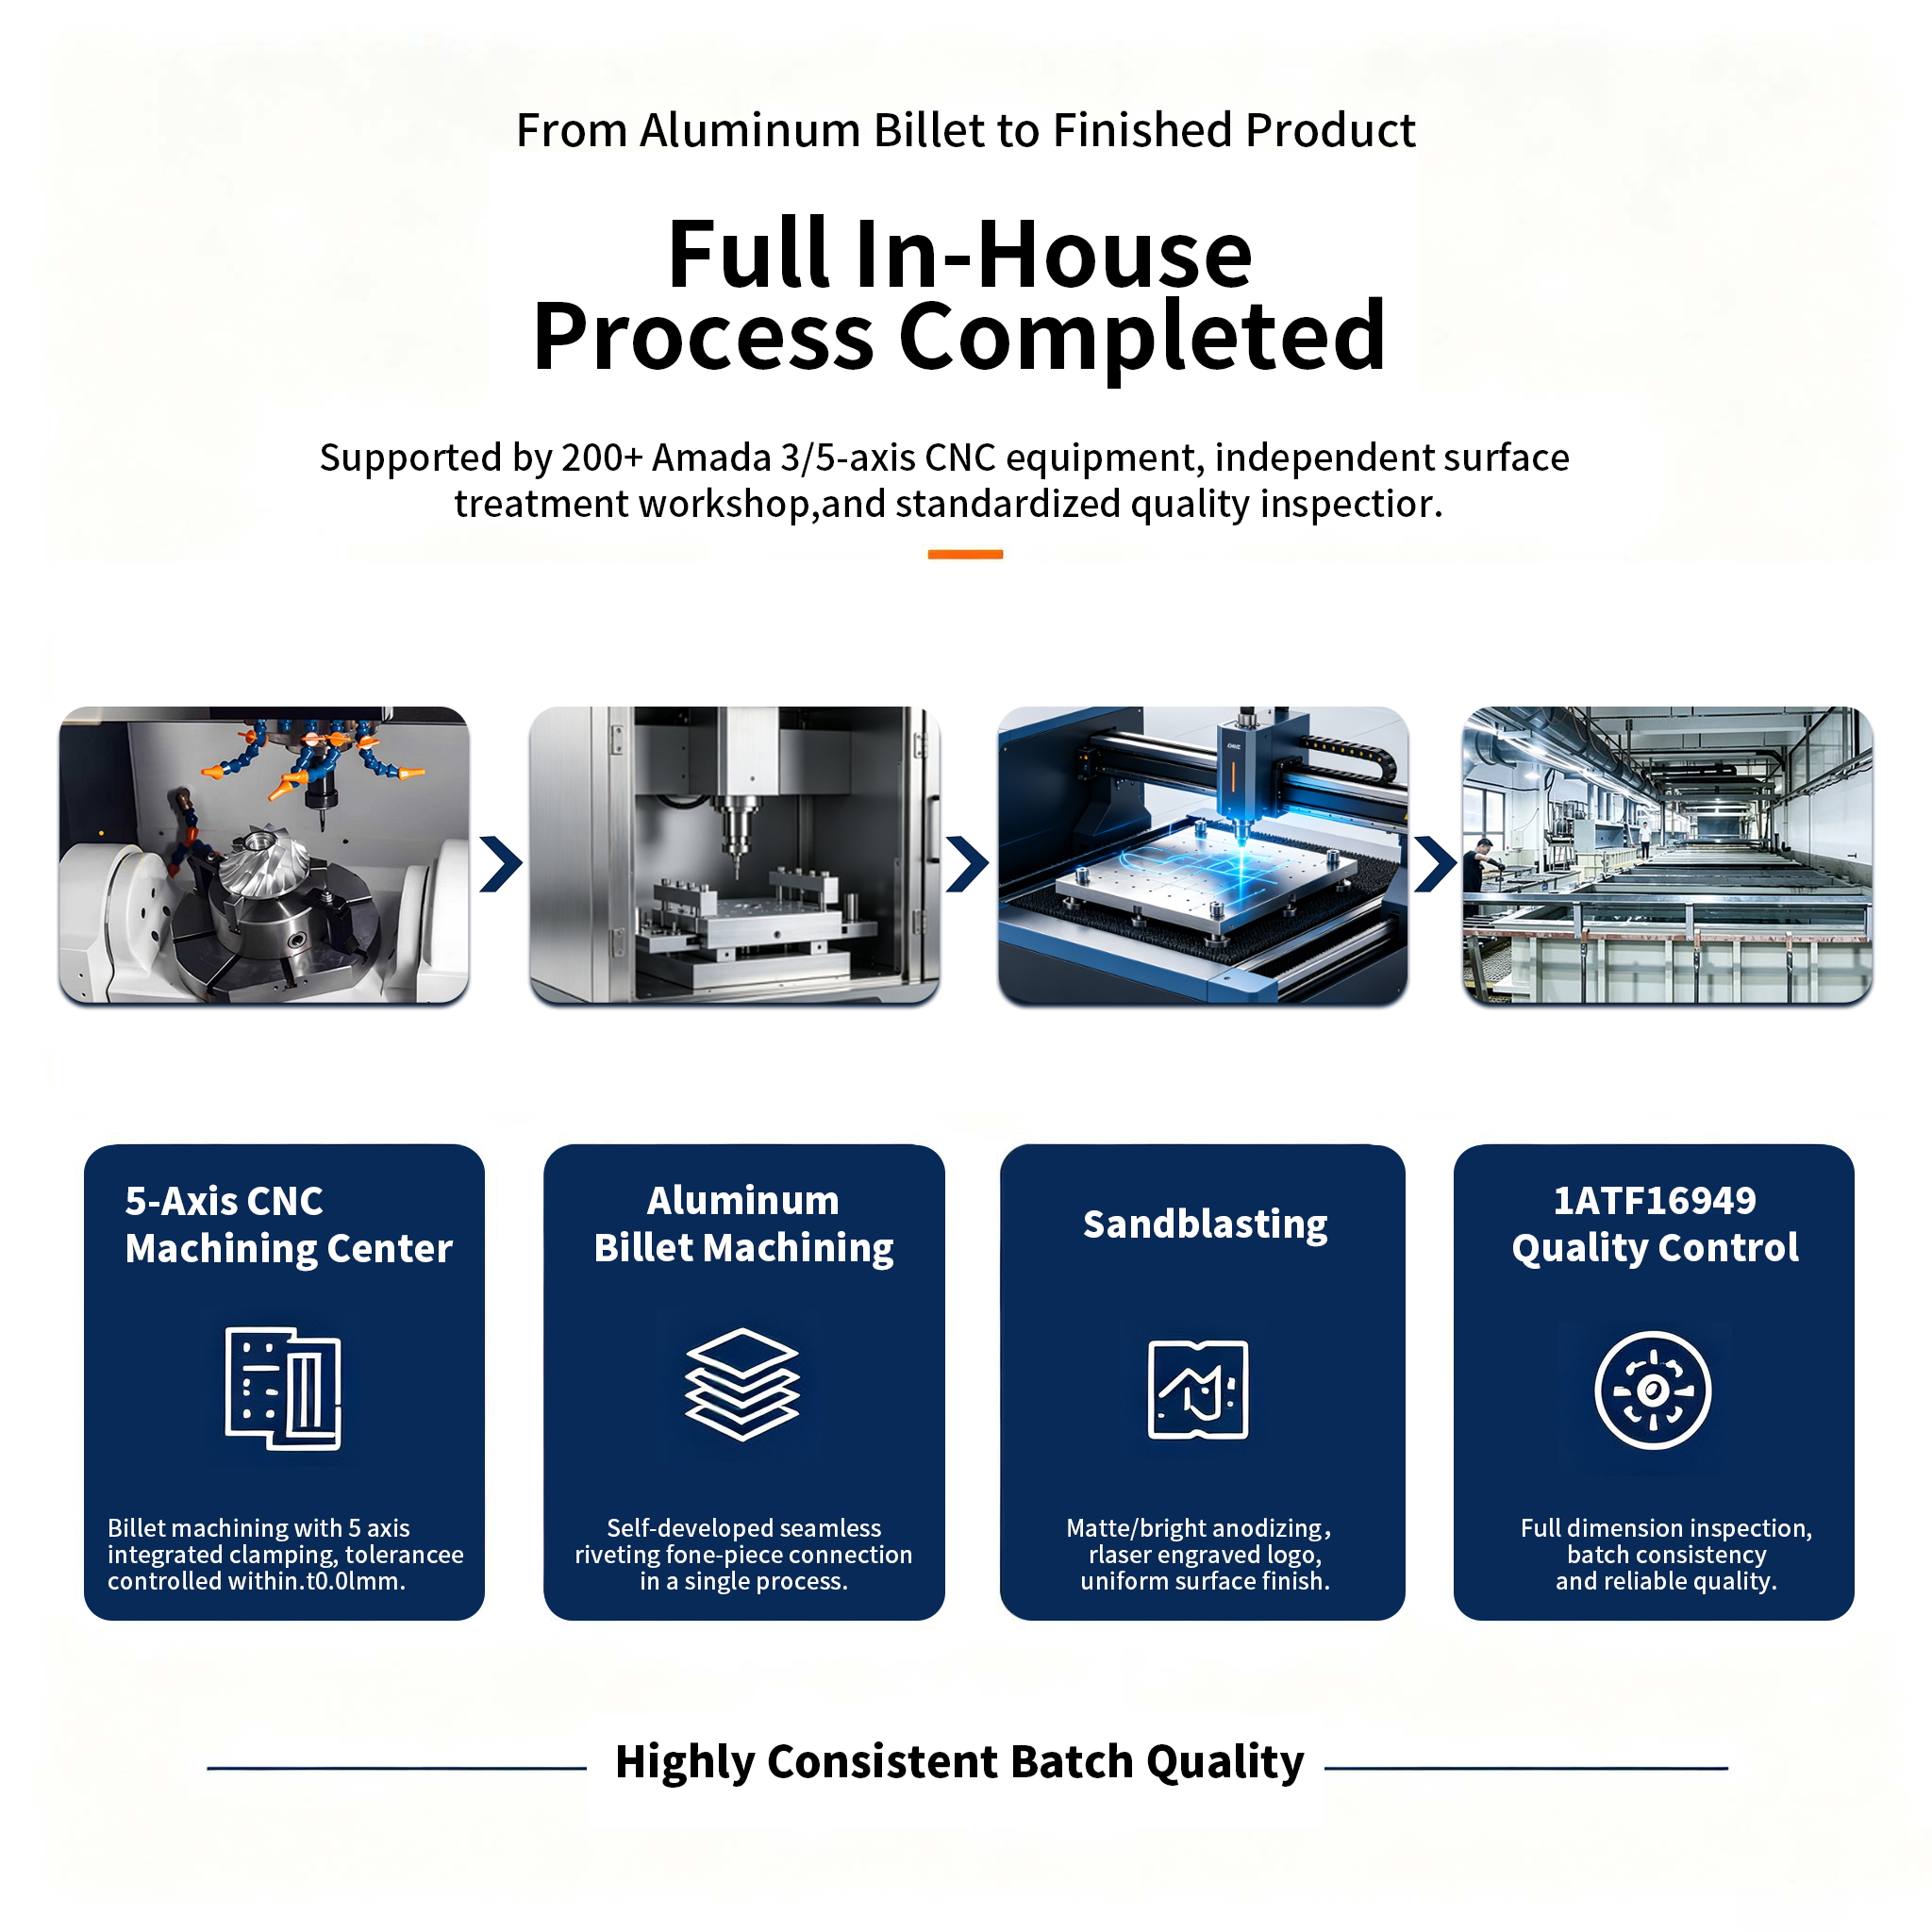
From aluminum billet to finished product — 200+ Amada 3/5-axis CNC machines, independent surface workshop, standardized QC.
Our engineers developed this process in-house. The nut column is pressed inward and sealed inside the material — watch how the backplate stays perfectly flat with zero marks.
Quality Assurance
Every key specification is verified with CMM, surface gauge and colorimeter on every production batch — data archived per lot for full traceability.
| Specification | Requirement | Achieved | Method |
|---|---|---|---|
| Backplate flatness | Fully flat, zero rivet marks | 100% pass | Visual + surface gauge |
| Machining tolerance | ±0.01 mm | ±0.01 mm | CMM measurement |
| Rivet joint strength | Meets OEM pull-out spec | Passed | Pull-out test |
| Anodizing color | ΔE < 1.5 vs. master | ΔE < 1.0 avg | Colorimeter |
| Salt spray resistance | 72 h, no corrosion | Passed | ASTM B117 |
| Batch consistency | 100% dimension inspection | 100% pass | Full dimension CMM |
Why Rejin CNC
The brand compared us against shops in three countries. Here is what closed the deal.
vs. standard riveting
Zero through-holes, flat backplate, stronger joint — a process customers cannot get from commodity shops, protected by years of in-house refinement.
vs. outsourced finishing
Machining, sandblasting, anodizing and laser marking under one roof — no hand-offs, no color drift, no third-party excuses.
vs. batch sampling
Critical dimensions measured on every part, every batch verified — defects never ship to your line.
vs. sales-led support
You talk directly to the people who run the machines and the process — technical answers in hours, DFM in 48.
Project Results
The first batch fully met the brand’s standards, and the relationship has only grown since.
Customer Feedback
Direct quotes from the people who run this program on the customer side.
“The backplate is finally completely smooth. No rivet marks, no dents — it looks the way a premium product should.”
“Batch after batch, the anodizing color matches the reference sample. We stopped checking color on arrival.”
“Rejin’s DFM caught assembly issues our previous suppliers never mentioned. Delivery has been on time for three straight years.”
Free DFM Check · Quote in 24 Hours
Send us your CAD and get a free DFM check with a detailed quotation within 24 hours.