
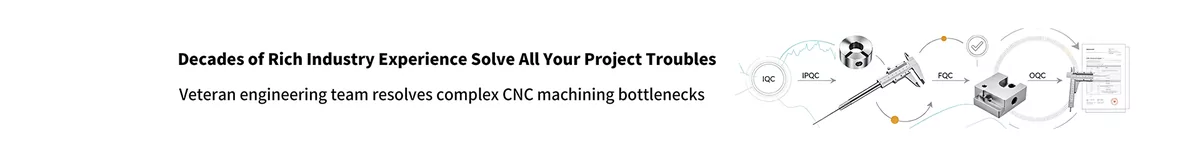
A vehicle fluid system needed corrosion-resistant connectors that held sealing under pressure cycles. Rejin CNC machined AISI 304 stainless steel connectors with integrated threads, stepped sealing shoulders and a concentric mounting base — every part full-dimension inspected, thread plug-gauge verified, and cleared for field testing on the first batch.
A real engineering story — the connector that had to hold fluid pressure, cycle after cycle, without a single leak.
In a vehicle fluid system, a connector is a promise: seal now, seal under pressure, seal after ten thousand cycles. This project began when an OEM’s fluid transfer module needed a corrosion-resistant connector solution — and their existing supplier could not hold thread engagement or sealing consistency.
The customer was upgrading a vehicle fluid transfer module that handled pressure cycles and long-term sealing. The connectors had to be machined from AISI 304 stainless steel, with integrated internal threads, stepped sealing shoulders and a concentric mounting base — geometry that is easy to draw and hard to machine repeatably. A small pilot batch was sourced to verify machining accuracy and thread fit before scaling to mass production.
The pilot from the incumbent supplier failed on the bench: thread engagement was inconsistent, sealing faces showed measurable runout, and a percentage of parts leaked under pressure testing. The customer needed a shop that treated thread geometry and concentricity as sealing-critical features — not cosmetic ones.
Rejin CNC’s automotive team reviewed the drawing with a DFM-first approach: material behavior in threading, sealing-shoulder geometry, and the inspection plan that would prove the part rather than assume it. We proposed optical profile measurement and thread plug-gauge verification on every part — full-dimension inspection as standard, not as a premium.
How the pilot batch changed the program. The first batch arrived with every part optically profiled and thread plug-gauge verified. Thread engagement was smooth with no looseness or cross-thread issues. Sealing surfaces showed consistent concentricity in measurement. No leakage or pressure-fit loss occurred during validation. The batch required no additional adjustments and was cleared directly for field testing — the customer’s first connector pilot to pass first time.
Six problems that failed the previous pilot batch before Rejin CNC.
Parts leaked under pressure testing — sealing faces showed measurable runout that no drawing tolerance had caught.
Threads varied between parts — some engaged smoothly, others loosened or cross-threaded during assembly.
Sealing shoulders were not concentric with the thread axis, breaking the seal under pressure cycling.
Inconsistent surface finish on stainless parts raised corrosion risk in demanding automotive environments.
Connectors could not hold sealing across repeated pressure cycles — the core requirement of the module.
Inspection was sampled and partial — the customer could not prove part quality for the whole batch.
CNC-machined connectors in AISI 304 stainless steel — integrated internal threads, stepped sealing shoulders and a concentric mounting base — engineered for pressure cycles and long-term sealing, with full-dimension inspection and thread plug-gauge verification on every part.
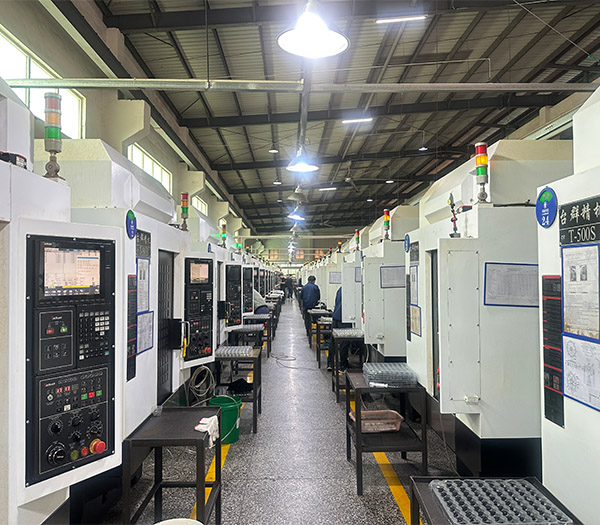
The difference was never a single feature — it was a complete sealing-critical machining system.
Corrosion-resistant, pressure-rated body — the right grade for vehicle fluid systems demanding long-term reliability.
Precision thread machining with controlled engagement — smooth, consistent, no looseness or cross-threading.
Machined sealing shoulders provide a positive sealing surface, held concentric with the thread axis.
Single-setup machining keeps the mounting base, threads and sealing faces on one axis — consistent in every measurement.
Full-dimension inspection with optical profile measurement on every part — geometry proven, not assumed.
Every thread verified with a plug gauge for engagement and fit — a sealing-critical feature checked as a feature.
Real problems from the automotive machining floor — root cause, fix, and the result we hold today.
Every step is documented with in-process inspection, so sealing reliability is built in — not checked in at the end.
AISI 304 stainless steel bar stock selected for corrosion resistance and pressure-rated performance in vehicle fluid systems.
Turning, milling and threading in single setups keep threads, sealing shoulders and base concentric on one axis.
Controlled finishing passes produce clear, well-defined threads and smooth sealing faces for reliable engagement.
Precision deburring and ultrasonic cleaning remove micro-burrs that could compromise sealing or contamination.
Optical profile measurement plus thread plug-gauge verification on every part — geometry proven per lot.
Parts individually packed, rust-protected and documented to arrive ready for system-level assembly.
Stainless connectors — threads, sealing shoulders and concentricity verified on every part.
If the sealing shoulder runs out relative to the thread axis, the seal breaks under pressure — no matter how good the thread is. Single-setup machining and per-part measurement are what make leak-free sealing repeatable, batch after batch.
Every key specification is verified on every production batch — data archived per lot for full traceability.
| Specification | Requirement | Achieved | Method |
|---|---|---|---|
| Thread engagement | Smooth, no looseness | 100% pass | Thread plug-gauge |
| Sealing shoulder concentricity | Per drawing | Consistent | Optical profile |
| Internal thread fit | GO/NO-GO | 100% pass | Plug-gauge set |
| Leakage test | No leakage | No leakage | Pressure validation |
| Pressure-fit loss | None | None | Pressure cycling |
| Batch consistency | Full-dimension check | 100% pass | Optical profile + gauge |
The customer compared us against the incumbent supplier. Here is what closed the deal.
Every part is optically profiled and thread plug-gauge verified — quality proven for the whole batch, not assumed from a sample.
Threads, sealing shoulders and base machined on one axis — the geometry that makes leak-free sealing repeatable.
We treat thread and concentricity as sealing features — designed, machined and measured as such, not as cosmetic details.
You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks.
The first pilot batch passed every validation gate — and cleared for field testing without a single adjustment.
Direct quotes from the people who validated this program on the customer side.
“Every thread was plug-gauge verified — we could see the whole batch was right, not hope a sample was.”
“No leakage, no pressure-fit loss, no adjustments. It was the first pilot batch we cleared without rework.”
“The single-setup concentricity thinking is exactly what our sealing application needed. It shows in the measurements.”
Send us your CAD and get a free DFM check with a detailed quotation within 24 hours.
Your message lands directly with our senior engineers — instantly acknowledged.
We study your requirements and propose a workable solution with material & process options.
Detailed quotation with specs, options and lead time — no hidden fees.
Approve the sample, then we mass-produce with full QC and on-time shipping.
WhatsApp: +86 13790500374
Email: info@rejincnc.com
Your CAD files are kept strictly confidential. Quotation within 24 hours.