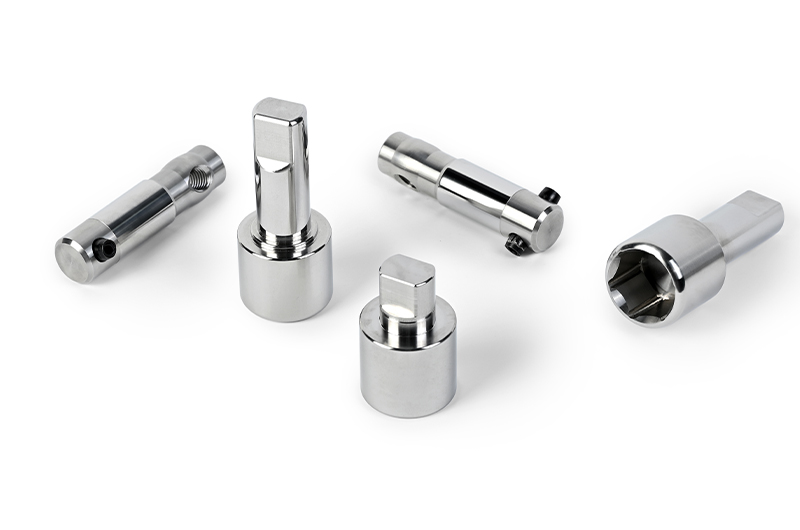
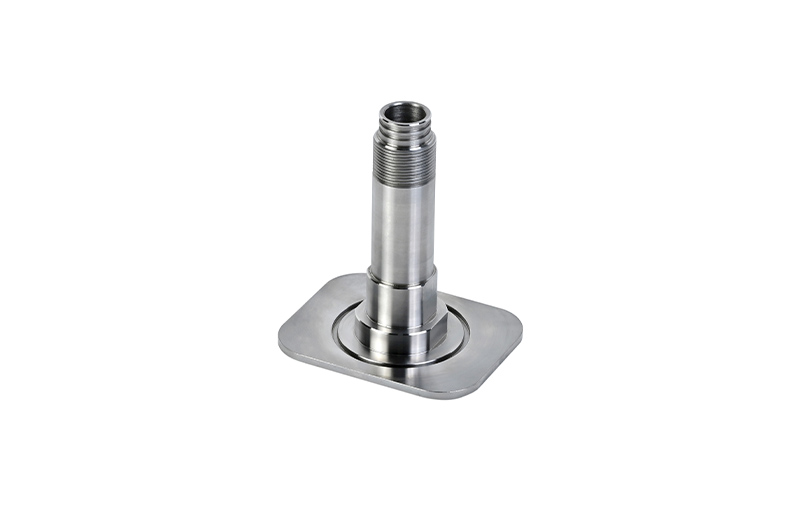
Studi kasus permesinan CNC, studi kasus suku cadang presisi

Didukung oleh standar ISO9001 & IATF16949 untuk pengendalian mutu proses penuh, kami menugaskan manajer proyek berpengalaman untuk menangani semua tantangan dan kesulitan teknis proyek OEM Anda.
Kami memajukan manufaktur CNC hijau berkelanjutan, dan menyediakan suku cadang logam presisi yang disesuaikan untuk perusahaan-perusahaan terkemuka global dengan dukungan ujung-ke-ujung yang andal.
Kotak Audio yang Dibuat dengan Mesin CNC Kustom dengan Pemasangan Paku Keling Tanpa Sambungan

Kotak Audio yang Dibuat dengan Mesin CNC Kustom dengan Pemasangan Paku Keling Tanpa Sambungan

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important}body .produc-banner{display:none!important}.rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px}.rjc-wrap *{box-sizing:border-box}.rjc-wrap img{max-width:100%;height:auto}.rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600}.rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5}.rjc-wrap h2{font-size:32px;margin:0 0 8px}.rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px}.rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto}.rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/Custom-CNC-Machined-Audio-Enclosures-with-Embedded-Seamless-Riveting.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)}.rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2}.rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none}.rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none}.rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)}.rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px}.rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px}.rjc-hero-left{max-width:780px}.rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3}.rjc-viz-b1{top:14%;right:6%}.rjc-viz-b2{bottom:20%;right:6%}.rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px}.rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase}.rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px}.rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)}.rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85}.rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px}.rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px}.rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px}.rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1}.rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)}.rjc-cta:hover::after{transform:translateX(4px)}.rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px}.rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1}.rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)}.rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px}.rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none}.rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none}.rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1}.rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1}.rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1}.rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1}.rjc-sec{margin-bottom:48px}.rjc-sec-head{text-align:center;margin-bottom:32px}.rjc-sec-head .rjc-sub{margin-top:6px}.rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center}.rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)}.rjc-list{margin:16px 0 0;padding:0;list-style:none}.rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px}.rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px}.rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px}.rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease}.rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)}.rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px}.rjc-card h3{font-size:18px;margin:0 0 8px}.rjc-card p{font-size:14px;margin:0;color:#6b6f7a}.rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px}.rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7}.rjc-story strong{color:#1C2333}.rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0}.rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start}.rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center}.rjc-pain h3{font-size:16px;margin:0 0 4px}.rjc-pain p{font-size:14px;margin:0;color:#6b6f7a}.rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px}.rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px}.rjc-sol h3{font-size:16px;margin:0 0 6px}.rjc-sol p{font-size:14px;margin:0;color:#6b6f7a}.rjc-challs{display:grid;gap:18px}.rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px}.rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px}.rjc-chall h3{font-size:18px;margin:0}.rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px}.rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c}.rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px}.rjc-ch-line b.pr{color:#D64545}.rjc-ch-line b.fx{color:#4376FB}.rjc-ch-line b.rs{color:#2E9E5B}.rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB}.rjc-diff-item h3{font-size:16px;margin:0 0 6px}.rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a}.rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px}.rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep}.rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7}.rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1}.rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px}.rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px}.rjc-step p{font-size:14px;margin:0;color:#6b6f7a}.rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)}.rjc-table{width:100%;border-collapse:collapse;font-size:14.5px}.rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase}.rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c}.rjc-table tr:nth-child(even) td{background:#FAFBFF}.rjc-table td:first-child{font-weight:500;color:#1C2333}.rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff}.rjc-results h2{color:#fff}.rjc-results .rjc-sub{color:#aeb6cc}.rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px}.rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center}.rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600}.rjc-res b em{font-style:normal;color:#4376FB}.rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4}.rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px}.rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px}.rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333}.rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px}.rjc-media{border-radius:14px;overflow:hidden;box-shadow:0 12px 34px rgba(28,35,51,.16);background:#000;margin-top:22px}.rjc-media img{display:block;width:100%;height:auto;border-radius:14px}.rjc-cap{font-size:12.5px;color:#8a8f9c;text-align:center;margin:10px 0 0}.rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s}.rjc-btn:hover{background:#1C2333;color:#fff}.rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)}.rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff}@media (max-width:991px){.rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/Custom-CNC-Machined-Audio-Enclosures-with-Embedded-Seamless-Riveting.jpg') center/cover no-repeat}.rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px}.rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px}.rjc-2col{grid-template-columns:1fr;gap:24px}.rjc-cards,.rjc-steps{grid-template-columns:1fr}.rjc-res-grid{grid-template-columns:repeat(2,1fr)}.rjc-quotes{grid-template-columns:1fr}.rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr}.rjc-chall .rjc-ch-lines{grid-template-columns:1fr}}@media (max-width:575px){.rjc-stats{grid-template-columns:1fr 1fr;gap:10px}.rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px}.rjc-cta-sec{padding:36px 22px}} Embedded RivetingSelf-Developed Process IATF 16949Certified Production CNC Machining Case Study · Audio Equipment CNC Audio Enclosures with Embedded Seamless Riveting — Zero Backplate Rivet Marks A European audio brand spent months rejecting enclosures with visible rivet marks on the backplate. Rejin CNC’s self-developed embedded seamless riveting delivers a fully flat back with zero through-holes — machined to ±0.01 mm, anodized in-house, and IATF 16949 verified at volume. See How We Solved ItGet a Free DFM Review 0Rivet marks on backplate — fully flat surface ±0.01 mmDimensional tolerance, CMM verified 200+Amada 3/5-axis CNC machines in-house IATF 16949Certified production & quality control The Story How This Project Really Began A real engineering story — a visible flaw, three failed suppliers, and the process that fixed it. Some of the best engineering stories start with a tiny visible flaw. For a European audio brand preparing to launch a new analog amp simulator, the flaw sat right on the backplate: rows of raised rivet marks that made a premium product look cheap. The product was a compact guitar amp simulator — designed in France, sold worldwide. The industrial design was clean: a brushed aluminum housing with laser-marked control graphics, engineered for the tone-focused musicians who would buy it. On the front, the product looked flawless. On the back, traditional through riveting left raised dents where rivets penetrated the aluminum plate. Every unit carried the marks, and every unit undermined the premium look the brand had spent years building. For months, the brand’s sourcing team searched for a better answer. They evaluated machine shops in three countries. Some shops said the marks were unavoidable — “that’s just how riveting works.” Others offered to hide the marks with stickers or paint, which the engineers rejected outright. One supplier quoted a cheaper die-cast alternative that changed the product’s weight, feel and cost. None of them solved the real problem. Then the brand’s team was referred to Rejin CNC. Instead of quoting the drawing as-is, our engineers ran a free DFM review and proposed something the other shops had never mentioned: an embedded seamless riveting process — nut columns pressed inward from the back, sealed inside the material, with zero through-holes and a completely flat backplate. No marks. No dents. No stickers. “The backplate is the face nobody talks about — until it ruins the product.” How the first sample changed everything. The first article arrived with a backplate so flat that the customer’s quality team ran their fingers across it twice to confirm. Dimension checks passed on the first pass. Assembly fit was perfect. The embedded rivet structure passed pull-out testing with margins to spare. That first article became the reference baseline for every batch that followed — and the brand never looked back. The Customer’s Pain Points Why Previous Suppliers Could Not Deliver Six problems that every candidate shop failed to solve before Rejin CNC. 1 Visible rivet marks Through rivets left raised dents on the backplate — every single unit carried the marks that broke the clean surface. 2 Cheap premium look The dents made a high-end audio product look low-cost on retail shelves, directly hurting the brand’s positioning. 3 Weak joint confidence Rivets penetrating the plate compromised structural integrity and risked clearance issues with internal electronics. 4 Anodizing inconsistency Color drifted between batches, and marks became even more visible after coating — two problems in one finish. 5 No engineering feedback Suppliers quoted drawings as-is and called rivet marks “unavoidable” instead of proposing a better process. 6 Unreliable scale-up Shops handled samples but lost quality or deadlines when production ramped to volume. Project Overview Audio Equipment Enclosures with Seamless Backplates for Global Audio Brands CNC-machined aluminum housings for audio equipment — amp simulators, sound cards and audio interfaces — built around Rejin CNC’s self-developed embedded seamless riveting: a fully flat backplate with zero rivet marks, one-piece structure and optimized strength. 6063-T5 extruded aluminum, precision CNC machined with 5-axis integrated clamping Embedded seamless riveting — one-piece connection, zero through-holes Matte/bright anodizing with laser-engraved logos, uniform finish ±0.01 mm dimensional tolerance, CMM verified on every batch IATF 16949 quality system, from prototype to mass production Traditional through riveting vs. our embedded seamless process — appearance and strength both optimized. Our Engineering Solution How We Engineered the Part for Repeatable Production The difference was never a single machine — it was a complete engineering system built around one process. Riveting Embedded Seamless Riveting Nut columns are pressed inward and sealed inside the material in a single operation — no through-holes, no raised marks, and a fully flat backplate that passes the fingertip test every time. Machining 5-Axis One-Piece Clamping Billet machining with 5-axis integrated clamping holds thin-wall geometry without distortion, keeping tolerance within ±0.01 mm on critical features. Surface In-House Sandblasting & Anodizing Matte or bright anodizing with laser-engraved logos runs under our own roof — uniform surface finish, no third-party hand-offs, no color drift. Inspection Full Dimension CMM Every critical feature is CMM-measured on every part, with data archived per production lot for full traceability. Quality IATF 16949 Process Control Standardized inspection and SPC keep batch consistency high — the same quality that automotive OEMs require, applied to audio hardware. Engineering DFM-First Approach We review your CAD before tooling, flag manufacturability issues, and design the process around the part — the review that won this customer is free for every project. Cutaway view — nut columns embedded inward, no through-hole, zero backplate marks. Why embedded riveting wins Standard riveting pushes rivets through the plate, leaving dents on the back and compromising internal component clearance. Our embedded process seats the nut column inside the material — the back stays smooth, the joint stays strong, and the product finally looks the way it should. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the production floor — root cause, fix, and the result we hold today. 🧱 Thin-Wall Distortion in Machining ProblemThin-wall sections warped during CNC machining, causing uneven gaps at assembly and inconsistent tolerance across parts. Fix5-axis integrated clamping holds the billet in one piece; low-stress toolpaths and separated rough/finish passes control heat and deflection. Result±0.01 mm tolerance held at volume — every part measures inside spec, batch after batch. 🔩 Rivet Pull-Down Marks on the Backplate ProblemStandard riveting pulled material and left visible dents — the exact flaw that failed three previous suppliers. FixSelf-developed embedded rivet die with controlled press force seats the nut column inward, sealing it inside the material with zero surface disturbance. ResultZero rivet marks on the backplate — fully flat surface confirmed by visual and surface-gauge inspection on every batch. 🎨 Anodizing Color Drift ProblemAnodizing color drifted between batches, and surface flaws became more visible after coating. FixIndependent in-house surface workshop with titrated bath chemistry, same-batch processing and colorimeter verification against a retained master sample. ResultUniform color across batches and years — parts from different months are visually indistinguishable. 🚚 Scaling Prototype to Mass Production ProblemThe launch plan demanded a sharp volume increase — most shops lose quality or lead time at that pace. FixDedicated machining cells, standardized fixtures, SPC on critical dimensions and a fixed shipping schedule agreed with the customer. Result100% batch consistency with on-time delivery — sustained for three straight years of production. Manufacturing Process From Aluminum Billet to Finished Enclosure in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 Aluminum Billet & Extrusion 6063-T5 aluminum billet is selected and extruded to near-net shape — stable material properties and lower machining stock for every run. 2 5-Axis CNC Machining Billet machining with 5-axis integrated clamping holds thin-wall geometry — tolerance controlled within ±0.01 mm on critical features. 3 Embedded Seamless Riveting Self-developed riveting joins the housing in a single process — nut columns embedded inward, zero through-holes, fully flat backplate. 4 Sandblasting Uniform matte surface prep removes machining traces and prepares the part for an even coating. 5 Anodizing & Laser Marking Matte or bright anodizing with laser-engraved logos — consistent color, sharp and fade-resistant graphics. 6 Full Inspection & Packing Full dimension CMM inspection, batch consistency check and protective packing before export — defects never ship. From aluminum billet to finished product — 200+ Amada 3/5-axis CNC machines, independent surface workshop, standardized QC. Embedded riveting hardware Our engineers developed this process in-house. The nut column is pressed inward and sealed inside the material — watch how the backplate stays perfectly flat with zero marks. Quality Assurance Measured Results, Not Promises Every key specification is verified with CMM, surface gauge and colorimeter on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Backplate flatness Fully flat, zero rivet marks 100% pass Visual + surface gauge Machining tolerance ±0.01 mm ±0.01 mm CMM measurement Rivet joint strength Meets OEM pull-out spec Passed Pull-out test Anodizing color ΔE < 1.5 vs. master ΔE < 1.0 avg Colorimeter Salt spray resistance 72 h, no corrosion Passed ASTM B117 Batch consistency 100% dimension inspection 100% pass Full dimension CMM Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The brand compared us against shops in three countries. Here is what closed the deal. vs. standard riveting Self-developed embedded riveting Zero through-holes, flat backplate, stronger joint — a process customers cannot get from commodity shops, protected by years of in-house refinement. vs. outsourced finishing 200+ machines + in-house surface workshop Machining, sandblasting, anodizing and laser marking under one roof — no hand-offs, no color drift, no third-party excuses. vs. batch sampling IATF 16949 + 100% inspection Critical dimensions measured on every part, every batch verified — defects never ship to your line. vs. sales-led support Engineers answer your questions You talk directly to the people who run the machines and the process — technical answers in hours, DFM in 48. Project Results What Three Years of Partnership Delivered The first batch fully met the brand’s standards, and the relationship has only grown since. 0Rivet marks on backplate — fully flat surface 100%Batch consistency, every lot verified ±0.01 mmHeld at volume, CMM verified 3+Years of stable mass production Customer Feedback What the OEM Buyers Say Direct quotes from the people who run this program on the customer side. “The backplate is finally completely smooth. No rivet marks, no dents — it looks the way a premium product should.” Product ManagerEuropean Audio Brand “Batch after batch, the anodizing color matches the reference sample. We stopped checking color on arrival.” Quality ManagerAudio Equipment OEM “Rejin’s DFM caught assembly issues our previous suppliers never mentioned. Delivery has been on time for three straight years.” Sourcing LeadGlobal Audio Brand Free DFM Check · Quote in 24 Hours Have a Similar CNC Enclosure or Audio Part Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();

Kotak Audio Aluminium 6063 Ekstrusi

Studi Kasus Kotak Audio yang Dibuat dengan Mesin CNC Kustom

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important} body .produc-banner{display:none!important} .rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px} .rjc-wrap *{box-sizing:border-box} .rjc-wrap img{max-width:100%;height:auto} .rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600} .rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5} .rjc-wrap h2{font-size:32px;margin:0 0 8px} .rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px} .rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto} .rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)} .rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2} .rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none} .rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none} .rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)} .rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px} .rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px} .rjc-hero-left{max-width:780px} .rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3} .rjc-viz-b1{top:14%;right:6%} .rjc-viz-b2{bottom:20%;right:6%} .rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px} .rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase} .rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px} .rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)} .rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85} .rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px} .rjc-stat{background:rgba(255,255,255,.08);border:1px solid rgba(255,255,255,.14);border-radius:12px;padding:18px 16px} .rjc-stat b{display:block;font-size:24px;color:#fff;font-weight:600;letter-spacing:.5px} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.4;display:block;margin-top:4px} .rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px} .rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px} .rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1} .rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)} .rjc-cta:hover::after{transform:translateX(4px)} .rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px} .rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1} .rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)} .rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px} .rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none} .rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none} .rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1} .rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1} .rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1} .rjc-sec{margin-bottom:48px} .rjc-sec-head{text-align:center;margin-bottom:32px} .rjc-sec-head .rjc-sub{margin-top:6px} .rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center} .rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)} .rjc-list{margin:16px 0 0;padding:0;list-style:none} .rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px} .rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px} .rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px} .rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease} .rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)} .rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px} .rjc-card h3{font-size:18px;margin:0 0 8px} .rjc-card p{font-size:14px;margin:0;color:#6b6f7a} .rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px} .rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7} .rjc-story strong{color:#1C2333} .rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0} .rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start} .rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center} .rjc-pain h3{font-size:16px;margin:0 0 4px} .rjc-pain p{font-size:14px;margin:0;color:#6b6f7a} .rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px} .rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px} .rjc-sol h3{font-size:16px;margin:0 0 6px} .rjc-sol p{font-size:14px;margin:0;color:#6b6f7a} .rjc-challs{display:grid;gap:18px} .rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px} .rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px} .rjc-chall h3{font-size:18px;margin:0} .rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px} .rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c} .rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px} .rjc-ch-line b.pr{color:#D64545} .rjc-ch-line b.fx{color:#4376FB} .rjc-ch-line b.rs{color:#2E9E5B} .rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB} .rjc-diff-item h3{font-size:16px;margin:0 0 6px} .rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a} .rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px} .rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep} .rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7} .rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1} .rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px} .rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px} .rjc-step p{font-size:14px;margin:0;color:#6b6f7a} .rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)} .rjc-table{width:100%;border-collapse:collapse;font-size:14.5px} .rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase} .rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c} .rjc-table tr:nth-child(even) td{background:#FAFBFF} .rjc-table td:first-child{font-weight:500;color:#1C2333} .rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff} .rjc-results h2{color:#fff} .rjc-results .rjc-sub{color:#aeb6cc} .rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px} .rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center} .rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600} .rjc-res b em{font-style:normal;color:#4376FB} .rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4} .rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px} .rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px} .rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333} .rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px} .rjc-cta{background:linear-gradient(135deg,#4376FB,#2f5be8);border-radius:16px;padding:48px 44px;text-align:center;color:#fff} .rjc-cta h2{color:#fff;font-size:28px;margin:0 0 10px} .rjc-cta p{color:#dbe4ff;margin:0 auto 26px;max-width:620px;font-size:15px} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap} .rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s} .rjc-btn:hover{background:#1C2333;color:#fff} .rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)} .rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff} @media (max-width: 991px){ .rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center/cover no-repeat} .rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px} .rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px} .rjc-stats{grid-template-columns:repeat(2,1fr)} .rjc-2col{grid-template-columns:1fr;gap:24px} .rjc-cards,.rjc-steps{grid-template-columns:1fr} .rjc-res-grid{grid-template-columns:repeat(2,1fr)} .rjc-quotes{grid-template-columns:1fr} .rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr} .rjc-chall .rjc-ch-lines{grid-template-columns:1fr} } @media (max-width: 575px){ .rjc-stats{grid-template-columns:1fr 1fr;gap:10px} .rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px} .rjc-cta{padding:36px 22px} } ±0.01 mmCMM Verified IATF 16949Certified Production CNC Machining Case Study · Premium Audio Custom CNC Machined Audio Enclosures — Held to ±0.01 mm, On Time Every Time A premium European audio brand spent eight months and twelve failed suppliers hunting for enclosures that held tolerance at volume. Rejin CNC machined their thin-wall 6063-T5 aluminum enclosure to ±0.01 mm — brushed, black-anodized and CMM-verified — then shipped 20,000+ units a month on schedule for three straight years. See How We Solved ItGet a Free DFM Review 6063-T5Aluminum alloy, extruded + precision CNC machined ±0.01 mmTolerance held at volume, CMM verified 20,000+Enclosures per month, prototype to mass production 100%On-time delivery, 3 years running The Story How This Project Really Began A real engineering story — the search, the failures, and the first DFM call that changed everything. Every difficult CNC project starts with a problem nobody else wants to solve. This one started in Germany, where a premium audio brand was preparing to launch a new generation of control units. The industrial design was stunning: a slim, minimalist enclosure in brushed, black-anodized aluminum. The engineering team loved it. The manufacturing team did not. The enclosure was compact, with wall sections as thin as 1.2 mm, visible surfaces that demanded a perfectly horizontal brushed texture, and a black anodized finish that had to stay color-stable across tens of thousands of parts. On paper, it looked like a routine CNC job. In reality, it was a test that most machine shops quietly failed. For eight months, the brand’s sourcing team searched. They evaluated machine shops in three countries, ordered sample parts from more than a dozen candidates. Some delivered accurate dimensions but rough, blotchy surfaces. Some produced a beautiful first article — and then could never repeat it at volume. One factory quoted an attractive price, quietly outsourced the anodizing to a third party, and the color drifted from batch to batch. Another could only run short runs of 500 parts, with no capacity to scale. Samples were good. Production was not. That is the classic gap in custom CNC machining, and it was costing the brand its entire launch calendar. “Send us your drawing, and we will tell you what is wrong with it before you spend a single dollar on tooling.” How Rejin CNC entered the picture. The brand’s sourcing team was referred to Rejin CNC by an industry contact. Instead of quoting the drawing as-is — the way every previous supplier had done — our engineers ran a free DFM review and came back with three pages of findings: two sharp internal corners that would create stress risers and risk cracking during anodizing, an undersized thread depth on the mounting boss, and a suggested wall-thickness adjustment that would cut distortion risk in half without changing the design language. The review took 48 hours. It was delivered before any purchase order existed. That single DFM review is what turned the conversation into a first sample order. The first article passed every single check on the customer’s list — dimension, surface, color, assembly fit. It did not just meet the standard; it set the baseline that every batch since has been measured against. The Customer’s Pain Points Why Previous Suppliers Could Not Deliver Six problems, repeated across more than a dozen candidate shops. 1 Anodizing color drift Black anodized batches drifted by ΔE > 3.0 against the master sample — unacceptable on a premium retail product where every unit must match. 2 Inconsistent brushed texture Brushing direction and depth varied from part to part and even within the same batch, ruining the “one continuous grain” look the design required. 3 Thin-wall distortion 1.2 mm wall sections warped during machining, leaving uneven gaps at assembly and forcing costly manual rework. 4 No scale-up capability Shops that handled 500-piece prototypes could not hold quality at 5,000, let alone 20,000+ units per month. 5 Unreliable lead times Missed ship dates and last-minute excuses forced the brand to keep unsafe inventory buffers and risk its retail calendar. 6 No engineering feedback Drawings were quoted as-is. Design issues surfaced only after tooling was cut and money was already spent. Project Overview Compact Control-Unit Enclosure for a European High-End Audio Brand A compact control-unit enclosure for a European high-end audio brand — engineered for precision fit, a horizontal brushed texture and color-stable black anodizing, produced from a single supplier with machining, finishing, laser marking and QC all in-house. 6063-T5 extruded aluminum + CNC machining, wall thickness down to 1.2 mm Horizontal brushed finish with color-stable black anodizing (ΔE < 1.5) Laser-marked panels with sharp, fade-resistant graphics Scaled from first article to 20,000+ units / month under SPC control 100% inspection on critical dimensions, every batch color-verified Our Engineering Solution How We Engineered the Part for Repeatable Production The difference was never a single machine — it was a complete engineering system built around one part. Material 6063-T5 Extruded Aluminum Extrusion gave us a near-net inner cavity and stable material properties run after run — lower machining stock, lower cost, and far better anodizing response than die-cast blanks other shops had proposed. Fixtures Zero-Distortion Clamping Custom vacuum fixtures and precision soft jaws hold every part identically without squeezing the 1.2 mm walls — the foundation of repeatable ±0.01 mm tolerance. Process Rough / Finish Separation Roughing removes stock and releases internal stress; parts settle; then finishing passes hold final geometry. Toolpaths are optimized for constant chip load and minimal tool deflection. Surface Controlled Brushing & Anodizing Dedicated brushing fixtures fix feed direction and pressure; anodizing bath chemistry is titrated per tank and color is verified against a retained master sample every batch. Inspection 100% Critical-Dimension CMM Key mounting and assembly features are measured on a CMM for every part in every batch — not sampled, not eyeballed — with data archived per production lot. Capacity Dedicated Cell, Planned Schedules A dedicated machining cell and fixed monthly production windows protect this program’s lead time, so the brand can commit dates to its retail calendar with confidence. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the production floor — root cause, fix, and the result we hold today. 🧱 Thin-Wall Distortion at 1.2 mm ProblemEarly samples warped 0.08–0.15 mm after machining — the clamp pressure and cutting heat deformed walls thinner than a credit card. FixRedesigned fixtures to vacuum-hold from the flat reference face, split roughing from finishing, added a settling period between the two, and dropped finishing feed rates to cut heat input. ResultFlatness held at 0.03 mm average — inside the customer’s 0.05 mm requirement — and assembly gaps became uniform across all batches. 🎯 One Continuous Brushed Grain ProblemHand-fed brushing left visible direction changes and depth differences between parts — the “one continuous grain” look broke across a batch of 500. FixBuilt dedicated brushing fixtures with a fixed feed path and constant pressure, and added a light-angle visual check to every inspection station. ResultBrushed texture consistency now passes 100% of visual + light-angle checks, and the customer has approved the standard as its reference for other projects. 🎨 Color-Stable Black Anodizing ProblemBlack anodizing drifted between batches — different dye uptake and tank age changed the black from warm to blue-ish, up to ΔE > 3.0. FixTitrated bath chemistry before every run, standardized rack loading and current density, and verified each batch against a retained master sample with a colorimeter. ResultBatch color now averages ΔE < 1.0 vs. master — well inside the ΔE < 1.5 requirement — and parts from different months are visually indistinguishable. 🚚 Scaling from Prototype to 20,000+ Units / Month ProblemThe customer’s launch plan demanded a 10× volume increase in one quarter — most shops lose control of quality or lead time at that pace. FixDedicated machining cell, parallel finishing and anodizing lines, SPC on critical dimensions, and a fixed weekly shipping schedule agreed with the customer. Result20,000+ units per month delivered with 100% on-time shipment and zero appearance-related complaints over three years of continuous production. Manufacturing Process From Drawing to Finished Enclosure in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 DFM & Fixture Design Engineers reviewed the CAD, optimized wall thickness and machining stock, then designed custom vacuum fixtures to hold every part identically — the foundation of repeatable tolerance. 2 CNC Machining 3-axis and 4-axis CNC milling centers rough and finish in separated operations, holding ±0.01 mm on critical features with constant chip-load toolpaths. 3 Deburring & Prep Automated and manual deburring removes edge marks, then parts are cleaned and prepped so the brushed texture comes out flawless. 4 Brushing & Black Anodizing Horizontal brushing gives the signature grain; sulfuric anodizing in a titrated bath produces a color-stable black, verified against the master sample. 5 Laser Marking Logos, model numbers and regulatory marks are laser-marked with fixture-located precision for sharp, fade-resistant graphics. 6 100% Inspection & Packing Every part is CMM-checked on critical dimensions, color-verified and individually wrapped to prevent scratches before export packaging. Quality Assurance Measured Results, Not Promises Every key specification is verified with CMM, profilometer and color measurement on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Machining tolerance ±0.01 mm ±0.01 mm CMM measurement Surface flatness 0.05 mm max 0.03 mm avg Height gauge / granite plate Anodizing color (black) ΔE < 1.5 vs. master ΔE < 1.0 avg Colorimeter Brushed texture Consistent grain direction 100% pass Visual + light-angle inspection Salt spray resistance 72 h, no corrosion Passed ASTM B117 Laser mark durability No fade after use Passed Abrasion / solvent test Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The brand compared us against shops in three countries. Here is what closed the deal. vs. quote-as-is shops DFM before the order We review the drawing and flag manufacturability issues before you spend on tooling — the review that first won this customer is free and standard for every project. vs. outsourced finishing Finishing 100% in-house Brushing, anodizing and laser marking run under our own roof — no hand-offs, no color drift, no third-party excuses between machining and the finished part. vs. batch sampling 100% inspection, not AQL sampling Critical dimensions are CMM-measured on every part and color is verified every batch, so a defect never ships to your line. vs. sales-led support Engineers answer your questions You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks. Project Results What Three Years of Partnership Delivered The first batch fully met the brand’s retail standards, and the relationship has only grown since. 0Appearance-related complaints from end users 100%On-time monthly deliveries, zero delays +20%Customer repurchase rate after metal upgrade 3Years of continuous production partnership Customer Feedback What the OEM Buyers Say Direct quotes from the people who run this program on the customer side. “We spent eight months looking for a partner who could hold both tolerance and surface finish at volume. Rejin’s first article passed everything — we stopped looking that day.” Purchasing DirectorEuropean Electronics Brand “The brushed texture and black anodizing are identical to our reference sample even after three years of production. Color has never been a discussion point on a single batch.” Quality ManagerEuropean Audio Brand “The metal material has an outstanding tactile feel. Customer repurchase rates increased by 20%, making them a key partner in our product upgrades.” Product ManagerNorth American Audio Equipment Supplier Free DFM Check · Quote in 24 Hours Have a Similar CNC Enclosure or Audio Part Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
Suku Cadang Otomotif dari Baja Tahan Karat 304

Proyek Suku Cadang Otomotif – Rakitan Konektor Baja Tahan Karat untuk Sistem Cairan Kendaraan

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important}body .produc-banner{display:none!important}.rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px}.rjc-wrap *{box-sizing:border-box}.rjc-wrap img{max-width:100%;height:auto}.rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600}.rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5}.rjc-wrap h2{font-size:32px;margin:0 0 8px}.rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px}.rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto}.rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/304-stainless-steel-Automotive-Parts.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)}.rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2}.rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none}.rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none}.rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)}.rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px}.rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px}.rjc-hero-left{max-width:780px}.rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3}.rjc-viz-b1{top:14%;right:6%}.rjc-viz-b2{bottom:20%;right:6%}.rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px}.rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase}.rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px}.rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)}.rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85}.rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px}.rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px}.rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px}.rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1}.rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)}.rjc-cta:hover::after{transform:translateX(4px)}.rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px}.rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1}.rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)}.rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px}.rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none}.rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none}.rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1}.rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1}.rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1}.rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1}.rjc-sec{margin-bottom:48px}.rjc-sec-head{text-align:center;margin-bottom:32px}.rjc-sec-head .rjc-sub{margin-top:6px}.rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center}.rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)}.rjc-list{margin:16px 0 0;padding:0;list-style:none}.rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px}.rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px}.rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px}.rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease}.rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)}.rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px}.rjc-card h3{font-size:18px;margin:0 0 8px}.rjc-card p{font-size:14px;margin:0;color:#6b6f7a}.rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px}.rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7}.rjc-story strong{color:#1C2333}.rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0}.rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start}.rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center}.rjc-pain h3{font-size:16px;margin:0 0 4px}.rjc-pain p{font-size:14px;margin:0;color:#6b6f7a}.rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px}.rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px}.rjc-sol h3{font-size:16px;margin:0 0 6px}.rjc-sol p{font-size:14px;margin:0;color:#6b6f7a}.rjc-challs{display:grid;gap:18px}.rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px}.rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px}.rjc-chall h3{font-size:18px;margin:0}.rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px}.rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c}.rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px}.rjc-ch-line b.pr{color:#D64545}.rjc-ch-line b.fx{color:#4376FB}.rjc-ch-line b.rs{color:#2E9E5B}.rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB}.rjc-diff-item h3{font-size:16px;margin:0 0 6px}.rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a}.rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px}.rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep}.rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7}.rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1}.rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px}.rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px}.rjc-step p{font-size:14px;margin:0;color:#6b6f7a}.rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)}.rjc-table{width:100%;border-collapse:collapse;font-size:14.5px}.rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase}.rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c}.rjc-table tr:nth-child(even) td{background:#FAFBFF}.rjc-table td:first-child{font-weight:500;color:#1C2333}.rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff}.rjc-results h2{color:#fff}.rjc-results .rjc-sub{color:#aeb6cc}.rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px}.rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center}.rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600}.rjc-res b em{font-style:normal;color:#4376FB}.rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4}.rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px}.rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px}.rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333}.rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px}.rjc-media{border-radius:14px;overflow:hidden;box-shadow:0 12px 34px rgba(28,35,51,.16);background:#000;margin-top:22px}.rjc-media img{display:block;width:100%;height:auto;border-radius:14px}.rjc-cap{font-size:12.5px;color:#8a8f9c;text-align:center;margin:10px 0 0}.rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s}.rjc-btn:hover{background:#1C2333;color:#fff}.rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)}.rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff}@media (max-width:991px){.rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/304-stainless-steel-Automotive-Parts.jpg') center/cover no-repeat}.rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px}.rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px}.rjc-2col{grid-template-columns:1fr;gap:24px}.rjc-cards,.rjc-steps{grid-template-columns:1fr}.rjc-res-grid{grid-template-columns:repeat(2,1fr)}.rjc-quotes{grid-template-columns:1fr}.rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr}.rjc-chall .rjc-ch-lines{grid-template-columns:1fr}}@media (max-width:575px){.rjc-stats{grid-template-columns:1fr 1fr;gap:10px}.rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px}.rjc-cta-sec{padding:36px 22px}} Sealing QualityThread & Concentricity Verified IATF 16949Certified Production CNC Machining Case Study · Automotive Stainless Steel Fluid Connectors for Vehicle Systems — Leak-Free Sealing at Every Thread A vehicle fluid system needed corrosion-resistant connectors that held sealing under pressure cycles. Rejin CNC machined AISI 304 stainless steel connectors with integrated threads, stepped sealing shoulders and a concentric mounting base — every part full-dimension inspected, thread plug-gauge verified, and cleared for field testing on the first batch. See How We Solved ItGet a Free DFM Review AISI 304Corrosion-resistant stainless body ±0.01 mmThread & sealing precision 100%Full-dimension inspected IATF 16949Certified production & QC The Story How This Project Really Began A real engineering story — the connector that had to hold fluid pressure, cycle after cycle, without a single leak. In a vehicle fluid system, a connector is a promise: seal now, seal under pressure, seal after ten thousand cycles. This project began when an OEM’s fluid transfer module needed a corrosion-resistant connector solution — and their existing supplier could not hold thread engagement or sealing consistency. The customer was upgrading a vehicle fluid transfer module that handled pressure cycles and long-term sealing. The connectors had to be machined from AISI 304 stainless steel, with integrated internal threads, stepped sealing shoulders and a concentric mounting base — geometry that is easy to draw and hard to machine repeatably. A small pilot batch was sourced to verify machining accuracy and thread fit before scaling to mass production. The pilot from the incumbent supplier failed on the bench: thread engagement was inconsistent, sealing faces showed measurable runout, and a percentage of parts leaked under pressure testing. The customer needed a shop that treated thread geometry and concentricity as sealing-critical features — not cosmetic ones. Rejin CNC’s automotive team reviewed the drawing with a DFM-first approach: material behavior in threading, sealing-shoulder geometry, and the inspection plan that would prove the part rather than assume it. We proposed optical profile measurement and thread plug-gauge verification on every part — full-dimension inspection as standard, not as a premium. “A thread is only as good as the runout behind it. Concentricity is what makes sealing repeatable.” How the pilot batch changed the program. The first batch arrived with every part optically profiled and thread plug-gauge verified. Thread engagement was smooth with no looseness or cross-thread issues. Sealing surfaces showed consistent concentricity in measurement. No leakage or pressure-fit loss occurred during validation. The batch required no additional adjustments and was cleared directly for field testing — the customer’s first connector pilot to pass first time. The Customer’s Pain Points Why the Incumbent Supplier Could Not Deliver Six problems that failed the previous pilot batch before Rejin CNC. 1 Sealing leakage Parts leaked under pressure testing — sealing faces showed measurable runout that no drawing tolerance had caught. 2 Inconsistent thread engagement Threads varied between parts — some engaged smoothly, others loosened or cross-threaded during assembly. 3 Concentricity drift Sealing shoulders were not concentric with the thread axis, breaking the seal under pressure cycling. 4 Corrosion risk Inconsistent surface finish on stainless parts raised corrosion risk in demanding automotive environments. 5 Pressure-cycle fatigue Connectors could not hold sealing across repeated pressure cycles — the core requirement of the module. 6 No full-dimension proof Inspection was sampled and partial — the customer could not prove part quality for the whole batch. Project Overview Stainless Steel Connector Assembly for Vehicle Fluid Systems CNC-machined connectors in AISI 304 stainless steel — integrated internal threads, stepped sealing shoulders and a concentric mounting base — engineered for pressure cycles and long-term sealing, with full-dimension inspection and thread plug-gauge verification on every part. Corrosion-resistant pressure-rated AISI 304 body High concentricity with clear, well-defined threads Stepped sealing shoulders for reliable sealing under pressure Full-dimension inspection incl. optical profile & thread plug-gauge No leakage, no pressure-fit loss — cleared for field testing Our Engineering Solution How We Engineered the Connector for Repeatable Sealing The difference was never a single feature — it was a complete sealing-critical machining system. Material AISI 304 Stainless Steel Corrosion-resistant, pressure-rated body — the right grade for vehicle fluid systems demanding long-term reliability. Threading Integrated Internal Threads Precision thread machining with controlled engagement — smooth, consistent, no looseness or cross-threading. Sealing Stepped Sealing Shoulders Machined sealing shoulders provide a positive sealing surface, held concentric with the thread axis. Concentricity Concentric Mounting Base Single-setup machining keeps the mounting base, threads and sealing faces on one axis — consistent in every measurement. Inspection Optical Profile Measurement Full-dimension inspection with optical profile measurement on every part — geometry proven, not assumed. Verification Thread Plug-Gauge Check Every thread verified with a plug gauge for engagement and fit — a sealing-critical feature checked as a feature. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the automotive machining floor — root cause, fix, and the result we hold today. 🔩 Thread Geometry Drift ProblemThread pitch and profile drifted between parts, causing loose or cross-threaded engagement. FixDedicated thread tools, controlled cutting parameters and in-process thread measurement. ResultThread engagement smooth and consistent — zero looseness or cross-thread issues across the batch. 🎯 Sealing-Face Concentricity ProblemSealing shoulders ran out relative to the thread axis — the leak source in the incumbent pilot. FixSingle-setup machining holds threads, shoulders and base on one axis; concentricity measured on every part. ResultSealing surfaces consistent in measurement — no leakage, no pressure-fit loss in validation. 🛡️ Pressure-Cycle Reliability ProblemConnectors must hold sealing across repeated pressure cycles — the core requirement of the module. FixMaterial grade, surface finish and sealing geometry engineered together for cyclic loading. ResultNo leakage or pressure-fit loss during validation — batch cleared directly for field testing. 🔬 Proving the Whole Batch ProblemSampled inspection could not prove quality for every part — a risk no automotive OEM accepts. FixFull-dimension inspection incl. optical profile and thread plug-gauge on every part, data per lot. Result100% verified batch — no additional adjustments needed, cleared directly for system-level assembly. Manufacturing Process From Bar Stock to Sealing Connector in 6 Controlled Steps Every step is documented with in-process inspection, so sealing reliability is built in — not checked in at the end. 1 Material Selection AISI 304 stainless steel bar stock selected for corrosion resistance and pressure-rated performance in vehicle fluid systems. 2 CNC Machining Turning, milling and threading in single setups keep threads, sealing shoulders and base concentric on one axis. 3 Thread & Sealing Finish Controlled finishing passes produce clear, well-defined threads and smooth sealing faces for reliable engagement. 4 Deburring & Cleaning Precision deburring and ultrasonic cleaning remove micro-burrs that could compromise sealing or contamination. 5 Full-Dimension Inspection Optical profile measurement plus thread plug-gauge verification on every part — geometry proven per lot. 6 Sealing-Ready Packaging Parts individually packed, rust-protected and documented to arrive ready for system-level assembly. Stainless connectors — threads, sealing shoulders and concentricity verified on every part. Why concentricity is a sealing feature If the sealing shoulder runs out relative to the thread axis, the seal breaks under pressure — no matter how good the thread is. Single-setup machining and per-part measurement are what make leak-free sealing repeatable, batch after batch. Quality Assurance Measured Results, Not Promises Every key specification is verified on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Thread engagement Smooth, no looseness 100% pass Thread plug-gauge Sealing shoulder concentricity Per drawing Consistent Optical profile Internal thread fit GO/NO-GO 100% pass Plug-gauge set Leakage test No leakage No leakage Pressure validation Pressure-fit loss None None Pressure cycling Batch consistency Full-dimension check 100% pass Optical profile + gauge Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The customer compared us against the incumbent supplier. Here is what closed the deal. vs. sampled inspection Full-dimension proof Every part is optically profiled and thread plug-gauge verified — quality proven for the whole batch, not assumed from a sample. vs. multi-setup shops Single-setup concentricity Threads, sealing shoulders and base machined on one axis — the geometry that makes leak-free sealing repeatable. vs. generic 304 work Sealing-critical thinking We treat thread and concentricity as sealing features — designed, machined and measured as such, not as cosmetic details. vs. sales-led support Automotive engineers answer You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks. Project Results What the Connector Program Delivered The first pilot batch passed every validation gate — and cleared for field testing without a single adjustment. 0Leaks or pressure-fit loss in validation 100%Thread plug-gauge verified 100%Concentricity consistent in measurement 1stBatch cleared directly for field testing Customer Feedback What the OEM Engineers Say Direct quotes from the people who validated this program on the customer side. “Every thread was plug-gauge verified — we could see the whole batch was right, not hope a sample was.” Fluid Systems EngineerAutomotive OEM “No leakage, no pressure-fit loss, no adjustments. It was the first pilot batch we cleared without rework.” Purchasing ManagerVehicle Systems Supplier “The single-setup concentricity thinking is exactly what our sealing application needed. It shows in the measurements.” Quality ManagerAutomotive OEM Free DFM Check · Quote in 24 Hours Have a Similar Automotive CNC Component Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore Auto CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
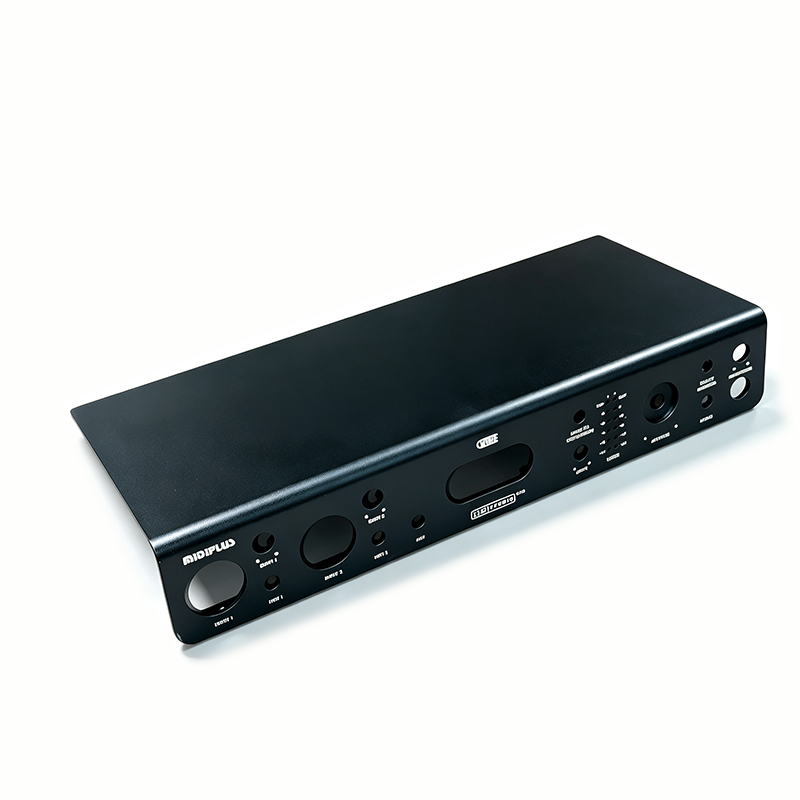
Komponen Bantalan Otomotif Baja Tahan Karat

Rakitan Poros-Selongsong Baja Tahan Karat yang Dibuat dengan Mesin Mikro untuk Perangkat Portabel

.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important}body .produc-banner{display:none!important}.rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px}.rjc-wrap *{box-sizing:border-box}.rjc-wrap img{max-width:100%;height:auto}.rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600}.rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5}.rjc-wrap h2{font-size:32px;margin:0 0 8px}.rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px}.rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto}.rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/Stainless-Steel-Automotive-Bearing-Components.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)}.rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2}.rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none}.rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none}.rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)}.rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px}.rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px}.rjc-hero-left{max-width:780px}.rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3}.rjc-viz-b1{top:14%;right:6%}.rjc-viz-b2{bottom:20%;right:6%}.rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px}.rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase}.rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px}.rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)}.rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85}.rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent}.rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px}.rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px}.rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px}.rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1}.rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)}.rjc-cta:hover::after{transform:translateX(4px)}.rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px}.rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1}.rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)}.rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px}.rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none}.rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none}.rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1}.rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1}.rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1}.rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1}.rjc-sec{margin-bottom:48px}.rjc-sec-head{text-align:center;margin-bottom:32px}.rjc-sec-head .rjc-sub{margin-top:6px}.rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center}.rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)}.rjc-list{margin:16px 0 0;padding:0;list-style:none}.rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px}.rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px}.rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px}.rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease}.rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)}.rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px}.rjc-card h3{font-size:18px;margin:0 0 8px}.rjc-card p{font-size:14px;margin:0;color:#6b6f7a}.rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px}.rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7}.rjc-story strong{color:#1C2333}.rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0}.rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start}.rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center}.rjc-pain h3{font-size:16px;margin:0 0 4px}.rjc-pain p{font-size:14px;margin:0;color:#6b6f7a}.rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px}.rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px}.rjc-sol h3{font-size:16px;margin:0 0 6px}.rjc-sol p{font-size:14px;margin:0;color:#6b6f7a}.rjc-challs{display:grid;gap:18px}.rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px}.rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px}.rjc-chall h3{font-size:18px;margin:0}.rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px}.rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c}.rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px}.rjc-ch-line b.pr{color:#D64545}.rjc-ch-line b.fx{color:#4376FB}.rjc-ch-line b.rs{color:#2E9E5B}.rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px}.rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB}.rjc-diff-item h3{font-size:16px;margin:0 0 6px}.rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a}.rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px}.rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep}.rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7}.rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1}.rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px}.rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px}.rjc-step p{font-size:14px;margin:0;color:#6b6f7a}.rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)}.rjc-table{width:100%;border-collapse:collapse;font-size:14.5px}.rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase}.rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c}.rjc-table tr:nth-child(even) td{background:#FAFBFF}.rjc-table td:first-child{font-weight:500;color:#1C2333}.rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff}.rjc-results h2{color:#fff}.rjc-results .rjc-sub{color:#aeb6cc}.rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px}.rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center}.rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600}.rjc-res b em{font-style:normal;color:#4376FB}.rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4}.rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px}.rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)}.rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px}.rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333}.rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px}.rjc-media{border-radius:14px;overflow:hidden;box-shadow:0 12px 34px rgba(28,35,51,.16);background:#000;margin-top:22px}.rjc-media img{display:block;width:100%;height:auto;border-radius:14px}.rjc-cap{font-size:12.5px;color:#8a8f9c;text-align:center;margin:10px 0 0}.rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s}.rjc-btn:hover{background:#1C2333;color:#fff}.rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)}.rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff}@media (max-width:991px){.rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2025/12/Stainless-Steel-Automotive-Bearing-Components.jpg') center/cover no-repeat}.rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px}.rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px}.rjc-2col{grid-template-columns:1fr;gap:24px}.rjc-cards,.rjc-steps{grid-template-columns:1fr}.rjc-res-grid{grid-template-columns:repeat(2,1fr)}.rjc-quotes{grid-template-columns:1fr}.rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr}.rjc-chall .rjc-ch-lines{grid-template-columns:1fr}}@media (max-width:575px){.rjc-stats{grid-template-columns:1fr 1fr;gap:10px}.rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px}.rjc-cta-sec{padding:36px 22px}} Micro Machining±0.01 mm Roundness SUS304Impact-Rated Body CNC Machining Case Study · Precision Components Micro-Machined Stainless Steel Shaft-Sleeve Assembly — ±0.01 mm Roundness for Drop-Impact Durability A portable diagnostic equipment maker needed a micro shaft-sleeve assembly that survived repeated drop impacts without binding or wearing loose. Rejin CNC machined SUS304 stainless steel sleeves to ±0.01 mm roundness — surface-hardened, full-dimension inspected, and small-batch flexible for fast design iteration. See How We Solved ItGet a Free DFM Review SUS304Stainless steel, impact & wear rated ±0.01 mmRoundness held, CMM verified 100%Full-dimension inspection IATF 16949Certified production & QC The Story How This Project Really Began A real engineering story — a component measured in microns, and the supplier who finally held the tolerance. Some components are so small you never see them — until they fail. The shaft-sleeve assembly in this project sits inside a portable device, where a few microns of wear or a hairline distortion turns smooth operation into wobble, binding and early failure. The customer was developing a new generation of portable diagnostic equipment — compact, battery-powered, built for field use, and designed to be carried and dropped far more often than it should be. The shaft-sleeve assembly had to carry a rotating load through thousands of cycles, resist shock from repeated drops, and hold its fit for the life of the device. On a component barely wider than a pencil lead, that is a demanding specification. The first supplier’s samples looked acceptable under a loupe. In testing, they failed: roundness drifted beyond spec, the sleeve bound against the shaft after a few dozen cycles, and drop impacts left the assembly loose. A second shop quoted a cheaper material that galled under load. Neither understood what micro CNC machining demands at this scale. The customer’s engineering team was then referred to Rejin CNC. Instead of quoting from the drawing alone, our engineers reviewed the assembly with a DFM-first eye: material selection, surface hardening for wear life, and a grinding strategy to hold roundness within ±0.01 mm — then proposed a small-batch production plan so the customer could iterate the design quickly before committing to volume. “In micro components, roundness is strength. A few microns decide whether a shaft lasts one drop or ten thousand.” How the first samples changed the program. The first batch arrived with roundness verified on every part — measured, not assumed. Drop-impact testing passed with margin, and assembly fit was consistent across all samples. The small-batch schedule let the customer validate three design iterations in six weeks instead of six months, and every iteration came back with the same precision. That first batch set the standard for everything that followed. The Customer’s Pain Points Why Previous Suppliers Could Not Deliver Six problems that failed two candidate shops before Rejin CNC. 1 Micro tolerance drift Sleeve roundness exceeded spec by microns, causing binding and uneven wear once assembled with the shaft. 2 Drop-impact failure Parts deformed or galled under shock loads, killing device reliability in real-world use. 3 Surface wear Soft untreated surfaces wore loose over cycles, shortening the assembly’s fit life and forcing early replacement. 4 Batch variation Dimensions drifted between runs, breaking assembly consistency and wasting engineering time on re-tolerance. 5 No small-batch flexibility Suppliers demanded large MOQs, making fast design iteration expensive and slow. 6 Limited engineering support No DFM feedback on micro features, material choice or surface treatment — problems surfaced only after parts arrived. Project Overview Micro Stainless Steel Shaft-Sleeve Assembly for Portable Device Systems A micro-machined shaft-sleeve assembly in SUS304 stainless steel, engineered for drop-impact resistance, micron-grade roundness and long-term fit life — produced with full in-house machining, surface hardening and 100% dimension inspection, from fast small-batch iteration to volume. SUS304 stainless steel, impact-resistant and wear-rated body Roundness controlled within ±0.01 mm, CMM verified Controlled surface hardness for extended wear life 100% full-dimension inspection with data per lot Small-batch supply for fast design validation and iteration Our Engineering Solution How We Engineered the Part for Repeatable Production The difference was never a single machine — it was a complete micro-machining system built around one assembly. Material SUS304 Stainless Steel Impact-resistant and wear-rated body — the right grade for shock loads, corrosion resistance and long fit life in compact mechanical systems. Machining Micro CNC Turning & Milling Precision micro geometries machined on dedicated 5-axis and turning centers, with low-stress toolpaths that protect thin-wall features. Roundness Grinding to ±0.01 mm Precision grinding after machining holds roundness within ±0.01 mm — verified on a CMM for every part, not sampled. Surface Controlled Surface Hardening Surface hardness controlled to spec for wear resistance, extending fit life through thousands of operating cycles. Inspection 100% Dimension Check Roundness, diameters and lengths measured on every part with data archived per production lot. Flexibility Small-Batch Production Flexible scheduling supports fast iteration and low-volume hardware testing before scaling to mass production. Challenges We Overcame Four Production Battles, and How We Won Each One Real problems from the micro-machining floor — root cause, fix, and the result we hold today. 🧱 Micro Thin-Wall Distortion ProblemThin-wall micro features warped under cutting forces — a few microns of distortion that failed roundness checks. FixLow-stress toolpaths, dedicated micro fixtures and separated rough/finish passes protect the geometry during machining. ResultRoundness held within ±0.01 mm on every part — verified on CMM, batch after batch. 🎯 Roundness Drift ProblemEarlier parts drifted out of round during finishing, causing binding with the mating shaft. FixPrecision grinding after CNC machining, with in-process measurement before final pass. Result±0.01 mm roundness held consistently — assembly fit remained smooth across all batches. 🛡️ Surface Wear & Galling ProblemUntreated surfaces galled under load, wearing loose after repeated cycles and shortening fit life. FixControlled surface hardening applied uniformly, with hardness verified per batch. ResultDrop-impact and wear testing passed with margin — no binding, no galling, no early failures. 🚚 Small-Batch Economics ProblemThe customer needed fast design iteration, but standard suppliers imposed large MOQs and long cycles. FixFlexible small-batch scheduling with dedicated changeover — three design iterations validated in six weeks. ResultFast iteration and validation at low cost — then a clean scale-up path when the design was frozen. Manufacturing Process From Bar Stock to Micro Sleeve in 6 Controlled Steps Every step is documented with in-process inspection, so quality is built in — not inspected in at the end. 1 Material Selection SUS304 stainless steel bar stock selected for impact resistance, corrosion resistance and machinability at micro scale. 2 Micro CNC Machining Precision turning and milling produce the micro geometry — bores, faces and bearing surfaces held with low-stress toolpaths. 3 Precision Grinding Grinding brings roundness and surface finish to ±0.01 mm spec with in-process measurement. 4 Surface Hardening Controlled surface treatment hardens the wear surface uniformly, extending fit life through thousands of cycles. 5 100% Dimension Inspection Roundness, diameters and lengths CMM-measured on every part — data archived per lot for traceability. 6 Anti-Corrosion Packaging Parts cleaned, rust-protected and individually packed to arrive ready for assembly. Micro stainless steel sleeves — roundness and finish verified on every part. Why micron-grade roundness matters A few microns of out-of-roundness means a shaft that binds, wobbles, or wears loose over time. Holding ±0.01 mm on every part is what turns a component into a reliable system — and it is the standard we held from the first sample to full production. Quality Assurance Measured Results, Not Promises Every key specification is verified on every production batch — data archived per lot for full traceability. Specification Requirement Achieved Method Roundness ±0.01 mm ±0.01 mm CMM measurement Critical diameters Per drawing 100% in spec CMM measurement Surface hardness Per wear spec Uniform Hardness tester Drop-impact resistance Pass testing Passed Impact test Salt spray resistance 48 h, no corrosion Passed ASTM B117 Batch consistency 100% dimension check 100% pass Full-dimension CMM Why Rejin CNC What Makes Us Different From a Commodity Machine Shop The customer compared us against shops that claimed micro capability. Here is what closed the deal. vs. quote-as-is shops DFM before the order We review the drawing and flag micro-feature, material and surface issues before you spend on tooling — free and standard for every project. vs. sampled inspection 100% dimension inspection Roundness and critical dimensions are CMM-measured on every part — a defect never ships to your line. vs. rigid MOQs Small-batch flexibility Fast iteration and low-volume hardware testing without large minimum order commitments — then a clean scale-up path. vs. sales-led support Engineers answer your questions You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks. Project Results What the Micro-Machining Program Delivered The first batch fully met the customer’s drop-impact and fit-life standards, and iteration has only gotten faster since. ±0.01 mmRoundness held on every part 100%Drop-impact tested and passed 0Binding or galled joints in field use 4×Faster design iteration vs. previous supplier Customer Feedback What the OEM Engineers Say Direct quotes from the people who run this program on the customer side. “The roundness is verified on every part — we stopped worrying about fit the moment the first batch arrived.” Mechanical LeadMedical Device OEM “We validated three design iterations in six weeks. No other supplier gave us that kind of speed with the same precision.” Product ManagerDiagnostic Equipment Brand “Drop-impact testing passed with margin on the first try. The surface hardening made a real difference to our reliability numbers.” Reliability EngineerMedical Device OEM Free DFM Check · Quote in 24 Hours Have a Similar Micro CNC Component Project? Send us your CAD and get a free DFM check with a detailed quotation within 24 hours. Get a Quote in 24 Hours →Explore CNC Capabilities (function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();
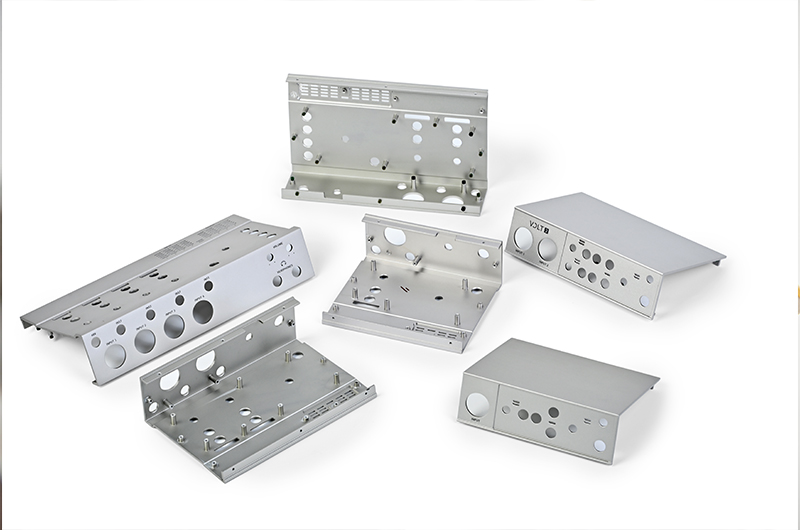
Produk
Kontak
WhatsApp
E-mail