.service-details-section{padding-top:0!important}.service-details-items{margin-top:0!important}.row.g-4{margin-top:0!important} body .produc-banner{display:none!important} .rjc-wrap{font-family:'Kanit',sans-serif;color:#555;line-height:1.75;font-size:16px} .rjc-wrap *{box-sizing:border-box} .rjc-wrap img{max-width:100%;height:auto} .rjc-wrap h1,.rjc-wrap h2,.rjc-wrap h3,.rjc-wrap h4{color:#1C2333;font-weight:600} .rjc-wrap h1{font-size:18px;font-weight:500;color:#7a7a7a;text-align:center;max-width:1200px;margin:24px auto 0;padding:0 24px;line-height:1.5} .rjc-wrap h2{font-size:32px;margin:0 0 8px} .rjc-kicker{display:inline-block;background:#4376FB;color:#fff;font-size:12px;font-weight:600;letter-spacing:1.5px;text-transform:uppercase;padding:5px 14px;border-radius:20px;margin-bottom:16px} .rjc-sub{color:#7a7a7a;font-size:15px;max-width:760px;margin:0 auto} .rjc-hero{background:linear-gradient(100deg,rgba(12,17,30,.95) 0%,rgba(17,24,42,.88) 40%,rgba(26,38,74,.66) 76%,rgba(38,58,116,.4) 100%),radial-gradient(820px 470px at 82% 10%,rgba(67,118,251,.24),transparent 62%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center 26%/cover no-repeat;border-radius:0;padding:0;min-height:calc(100vh - 90px);display:flex;align-items:center;color:#fff;position:relative;overflow:hidden;margin-bottom:56px;width:100vw;margin-left:calc(50% - 50vw);margin-right:calc(50% - 50vw)} .rjc-hero-inner{max-width:1200px;width:100%;margin:0 auto;padding:64px 48px;position:relative;z-index:2} .rjc-hero::before{content:"";position:absolute;width:620px;height:620px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-200px;right:-140px;z-index:1;pointer-events:none} .rjc-hero::after{content:"";position:absolute;width:400px;height:400px;border-radius:50%;border:1px solid rgba(255,255,255,.07);top:-70px;right:60px;z-index:1;pointer-events:none} .rjc-hero .rjc-kicker{background:rgba(67,118,251,.9);display:inline-block;padding:7px 18px;border-radius:40px;font-size:12px;font-weight:600;letter-spacing:2px;text-transform:uppercase;border:1px solid rgba(255,255,255,.22);box-shadow:0 4px 18px rgba(0,0,0,.18)} .rjc-hl{font-style:normal;color:#8FB2FF;background:linear-gradient(90deg,#BFD3FF,#6E9BFF);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-hero h2{color:#fff;font-size:44px;line-height:1.25;margin:12px 0 16px;max-width:820px} .rjc-hero p{color:#c6cde0;font-size:16px;max-width:760px;margin:0 0 32px} .rjc-hero-left{max-width:780px} .rjc-viz-badge{position:absolute;background:rgba(15,20,34,.82);backdrop-filter:blur(10px);border:1px solid rgba(255,255,255,.22);border-radius:14px;padding:12px 20px;box-shadow:0 14px 34px rgba(0,0,0,.45);z-index:3} .rjc-viz-b1{top:14%;right:6%} .rjc-viz-b2{bottom:20%;right:6%} .rjc-viz-badge b{display:block;font-size:17px;color:#fff;letter-spacing:.3px} .rjc-viz-badge span{display:block;font-size:11px;color:#93A5CE;margin-top:2px;letter-spacing:.6px;text-transform:uppercase} .rjc-stats{display:grid;grid-template-columns:repeat(4,1fr);gap:18px;margin-top:44px} .rjc-stat{background:rgba(255,255,255,.055);border:1px solid rgba(255,255,255,.13);border-radius:16px;padding:22px 18px 20px;position:relative;overflow:hidden;backdrop-filter:blur(8px);box-shadow:0 16px 40px rgba(0,0,0,.18),inset 0 1px 0 rgba(255,255,255,.08)} .rjc-stat::before{content:"";position:absolute;top:0;left:14%;right:14%;height:2px;background:linear-gradient(90deg,transparent,#6E9BFF,transparent);opacity:.85} .rjc-stat b{display:block;font-size:25px;font-weight:700;letter-spacing:.5px;background:linear-gradient(92deg,#FFFFFF 20%,#A8C0FF 90%);-webkit-background-clip:text;background-clip:text;-webkit-text-fill-color:transparent} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.45;display:block;margin-top:6px} .rjc-stat{background:rgba(255,255,255,.08);border:1px solid rgba(255,255,255,.14);border-radius:12px;padding:18px 16px} .rjc-stat b{display:block;font-size:24px;color:#fff;font-weight:600;letter-spacing:.5px} .rjc-stat span{font-size:12.5px;color:#aeb6cc;line-height:1.4;display:block;margin-top:4px} .rjc-cta-row{display:flex;gap:16px;flex-wrap:wrap;margin:0 0 36px} .rjc-cta{display:inline-flex;align-items:center;gap:10px;background:linear-gradient(135deg,#3D6BFF 0%,#5B8CFF 100%);color:#fff;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;box-shadow:0 10px 26px rgba(61,107,255,.4),inset 0 1px 0 rgba(255,255,255,.28);transition:transform .2s ease,box-shadow .2s ease;letter-spacing:.2px} .rjc-cta::after{content:"\2192";font-size:17px;transition:transform .2s ease;line-height:1} .rjc-cta:hover{transform:translateY(-2px);box-shadow:0 14px 34px rgba(61,107,255,.55),inset 0 1px 0 rgba(255,255,255,.28)} .rjc-cta:hover::after{transform:translateX(4px)} .rjc-cta-ghost{display:inline-flex;align-items:center;gap:10px;background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.34);color:#EAF0FF;font-weight:600;font-size:15px;padding:15px 32px;border-radius:10px;text-decoration:none;backdrop-filter:blur(8px);box-shadow:inset 0 1px 0 rgba(255,255,255,.14),0 6px 18px rgba(0,0,0,.18);transition:background .2s ease,border-color .2s ease,transform .2s ease;letter-spacing:.2px} .rjc-cta-ghost::after{content:"\2192";font-size:17px;line-height:1} .rjc-cta-ghost:hover{background:rgba(255,255,255,.15);border-color:rgba(255,255,255,.6);transform:translateY(-2px)} .rjc-cta-sec{background:radial-gradient(700px 320px at 85% -20%,rgba(67,118,251,.38),transparent 60%),radial-gradient(500px 300px at -10% 115%,rgba(67,118,251,.2),transparent 60%),linear-gradient(135deg,#141B2B 0%,#202A44 58%,#2E5BE0 155%);border-radius:18px;padding:64px 44px;text-align:center;position:relative;overflow:hidden;box-shadow:0 18px 48px rgba(28,35,51,.25);margin-bottom:56px} .rjc-cta-sec::before{content:"";position:absolute;width:380px;height:380px;border-radius:50%;border:1px solid rgba(255,255,255,.09);top:-150px;right:-90px;pointer-events:none} .rjc-cta-sec::after{content:"";position:absolute;width:230px;height:230px;border-radius:50%;border:1px solid rgba(255,255,255,.06);bottom:-95px;left:-55px;pointer-events:none} .rjc-cta-kicker{display:inline-block;background:rgba(67,118,251,.32);border:1px solid rgba(130,165,255,.45);color:#C7D8FF;font-size:12px;font-weight:600;letter-spacing:1.8px;text-transform:uppercase;padding:6px 18px;border-radius:30px;margin-bottom:20px;position:relative;z-index:1} .rjc-cta-sec h2{font-size:31px;color:#fff;margin:0 0 14px;line-height:1.3;position:relative;z-index:1} .rjc-cta-sec p{font-size:15.5px;color:#C6CEE0;max-width:640px;margin:0 auto 32px;line-height:1.7;position:relative;z-index:1} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap;position:relative;z-index:1} .rjc-sec{margin-bottom:48px} .rjc-sec-head{text-align:center;margin-bottom:32px} .rjc-sec-head .rjc-sub{margin-top:6px} .rjc-2col{display:grid;grid-template-columns:1.05fr .95fr;gap:40px;align-items:center} .rjc-2col img{border-radius:14px;box-shadow:0 12px 34px rgba(28,35,51,.16)} .rjc-list{margin:16px 0 0;padding:0;list-style:none} .rjc-list li{position:relative;padding:0 0 10px 30px;font-size:15px} .rjc-list li::before{content:"✓";position:absolute;left:0;top:0;width:20px;height:20px;background:#4376FB;color:#fff;font-size:12px;border-radius:50%;display:flex;align-items:center;justify-content:center;margin-top:2px} .rjc-cards{display:grid;grid-template-columns:repeat(3,1fr);gap:22px} .rjc-card{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:28px 24px;box-shadow:0 6px 20px rgba(28,35,51,.06);transition:transform .25s ease,box-shadow .25s ease} .rjc-card:hover{transform:translateY(-4px);box-shadow:0 14px 30px rgba(28,35,51,.12)} .rjc-card .rjc-ico{width:46px;height:46px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:22px;margin-bottom:16px} .rjc-card h3{font-size:18px;margin:0 0 8px} .rjc-card p{font-size:14px;margin:0;color:#6b6f7a} .rjc-story p{font-size:15.5px;color:#4a4f5c;margin:0 0 18px} .rjc-story .rjc-lead{font-size:17px;color:#1C2333;font-weight:500;line-height:1.7} .rjc-story strong{color:#1C2333} .rjc-pull{background:#F7F9FD;border-left:4px solid #4376FB;border-radius:0 12px 12px 0;padding:18px 24px;font-size:16px;color:#1C2333;font-weight:500;margin:22px 0} .rjc-pains{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-pain{display:flex;gap:14px;background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:18px 20px;align-items:flex-start} .rjc-pain .rjc-pn{width:34px;height:34px;min-width:34px;border-radius:50%;background:#FDEEEE;color:#D64545;font-weight:700;font-size:15px;display:flex;align-items:center;justify-content:center} .rjc-pain h3{font-size:16px;margin:0 0 4px} .rjc-pain p{font-size:14px;margin:0;color:#6b6f7a} .rjc-sols{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-sol{background:#F7F9FD;border:1px solid #eef1f7;border-radius:12px;padding:20px 22px} .rjc-sol .rjc-sn{display:inline-block;background:#4376FB;color:#fff;font-size:11px;font-weight:600;letter-spacing:1px;text-transform:uppercase;padding:3px 10px;border-radius:20px;margin-bottom:10px} .rjc-sol h3{font-size:16px;margin:0 0 6px} .rjc-sol p{font-size:14px;margin:0;color:#6b6f7a} .rjc-challs{display:grid;gap:18px} .rjc-chall{background:#fff;border:1px solid #e8ebf2;border-radius:14px;padding:26px 28px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-chall .rjc-ch-head{display:flex;align-items:center;gap:14px;margin-bottom:14px} .rjc-chall .rjc-ico{width:44px;height:44px;min-width:44px;border-radius:12px;background:#EEF3FF;color:#4376FB;display:flex;align-items:center;justify-content:center;font-size:21px} .rjc-chall h3{font-size:18px;margin:0} .rjc-chall .rjc-ch-lines{display:grid;grid-template-columns:1fr 1fr 1fr;gap:16px} .rjc-ch-line{background:#FAFBFF;border-radius:10px;padding:14px 16px;font-size:13.5px;color:#4a4f5c} .rjc-ch-line b{display:block;font-size:11.5px;letter-spacing:1px;text-transform:uppercase;margin-bottom:4px} .rjc-ch-line b.pr{color:#D64545} .rjc-ch-line b.fx{color:#4376FB} .rjc-ch-line b.rs{color:#2E9E5B} .rjc-diff{display:grid;grid-template-columns:1fr 1fr;gap:16px} .rjc-diff-item{background:#fff;border:1px solid #e8ebf2;border-radius:12px;padding:20px 22px;border-top:3px solid #4376FB} .rjc-diff-item h3{font-size:16px;margin:0 0 6px} .rjc-diff-item p{font-size:14px;margin:0;color:#6b6f7a} .rjc-diff-item .rjc-vs{display:inline-block;font-size:11px;font-weight:600;color:#8a8f9c;background:#F1F3F7;border-radius:20px;padding:2px 10px;margin-bottom:8px;letter-spacing:.5px} .rjc-steps{display:grid;grid-template-columns:repeat(3,1fr);gap:22px;counter-reset:rjcstep} .rjc-step{position:relative;background:#F7F9FD;border-radius:14px;padding:28px 24px 24px;border:1px solid #eef1f7} .rjc-step::before{counter-increment:rjcstep;content:"0" counter(rjcstep);position:absolute;top:-14px;right:18px;font-size:44px;font-weight:700;color:#4376FB;opacity:.16;line-height:1} .rjc-step h3{font-size:17px;margin:0 0 10px;display:flex;align-items:center;gap:10px} .rjc-step h3 .rjc-step-ic{width:34px;height:34px;min-width:34px;border-radius:9px;background:#4376FB;color:#fff;display:inline-flex;align-items:center;justify-content:center;font-size:16px} .rjc-step p{font-size:14px;margin:0;color:#6b6f7a} .rjc-table-wrap{background:#fff;border:1px solid #e8ebf2;border-radius:14px;overflow:hidden;box-shadow:0 6px 20px rgba(28,35,51,.06)} .rjc-table{width:100%;border-collapse:collapse;font-size:14.5px} .rjc-table th{background:#1C2333;color:#fff;text-align:left;padding:14px 20px;font-weight:500;font-size:13.5px;letter-spacing:.5px;text-transform:uppercase} .rjc-table td{padding:13px 20px;border-bottom:1px solid #eef1f7;color:#4a4f5c} .rjc-table tr:nth-child(even) td{background:#FAFBFF} .rjc-table td:first-child{font-weight:500;color:#1C2333} .rjc-results{background:linear-gradient(135deg,#1C2333,#2b3550);border-radius:16px;padding:44px 40px;color:#fff} .rjc-results h2{color:#fff} .rjc-results .rjc-sub{color:#aeb6cc} .rjc-res-grid{display:grid;grid-template-columns:repeat(4,1fr);gap:20px;margin-top:28px} .rjc-res{background:rgba(255,255,255,.07);border:1px solid rgba(255,255,255,.13);border-radius:12px;padding:22px 18px;text-align:center} .rjc-res b{display:block;font-size:30px;color:#fff;font-weight:600} .rjc-res b em{font-style:normal;color:#4376FB} .rjc-res span{font-size:13px;color:#aeb6cc;display:block;margin-top:6px;line-height:1.4} .rjc-quotes{display:grid;grid-template-columns:1fr 1fr 1fr;gap:22px} .rjc-quote{background:#fff;border:1px solid #e8ebf2;border-left:4px solid #4376FB;border-radius:12px;padding:26px 24px 22px;box-shadow:0 6px 20px rgba(28,35,51,.05)} .rjc-quote p{font-size:14.5px;font-style:italic;color:#4a4f5c;margin:0 0 14px} .rjc-quote .rjc-who{font-size:13.5px;font-weight:600;color:#1C2333} .rjc-quote .rjc-who span{display:block;font-weight:400;color:#8a8f9c;margin-top:2px} .rjc-cta{background:linear-gradient(135deg,#4376FB,#2f5be8);border-radius:16px;padding:48px 44px;text-align:center;color:#fff} .rjc-cta h2{color:#fff;font-size:28px;margin:0 0 10px} .rjc-cta p{color:#dbe4ff;margin:0 auto 26px;max-width:620px;font-size:15px} .rjc-cta-btns{display:flex;gap:16px;justify-content:center;flex-wrap:wrap} .rjc-btn{display:inline-block;background:#fff;color:#4376FB;font-weight:600;font-size:15px;padding:14px 36px;border-radius:30px;text-decoration:none;transition:all .25s} .rjc-btn:hover{background:#1C2333;color:#fff} .rjc-btn.rjc-btn-ghost{background:transparent;color:#fff;border:1.5px solid rgba(255,255,255,.55)} .rjc-btn.rjc-btn-ghost:hover{background:#fff;color:#4376FB;border-color:#fff} @media (max-width: 991px){ .rjc-hero{min-height:auto;padding:40px 26px;width:100%;margin-left:0;margin-right:0;background:linear-gradient(180deg,rgba(12,17,30,.96) 0%,rgba(14,20,36,.9) 100%),url('https://www.rejincnc.com/wp-content/uploads/2026/09/enclosure-v2.jpg') center/cover no-repeat} .rjc-stats{grid-template-columns:repeat(2,1fr);gap:12px;margin-top:34px} .rjc-viz-badge{display:none}.rjc-hero h2{font-size:29px} .rjc-stats{grid-template-columns:repeat(2,1fr)} .rjc-2col{grid-template-columns:1fr;gap:24px} .rjc-cards,.rjc-steps{grid-template-columns:1fr} .rjc-res-grid{grid-template-columns:repeat(2,1fr)} .rjc-quotes{grid-template-columns:1fr} .rjc-pains,.rjc-sols,.rjc-diff{grid-template-columns:1fr} .rjc-chall .rjc-ch-lines{grid-template-columns:1fr} } @media (max-width: 575px){ .rjc-stats{grid-template-columns:1fr 1fr;gap:10px} .rjc-res-grid{grid-template-columns:1fr 1fr;gap:12px} .rjc-cta{padding:36px 22px} }
±0.01 mmCMM Verified
IATF 16949Certified Production
CNC Machining Case Study · Premium Audio
Custom CNC Machined Audio Enclosures — Held to ±0.01 mm, On Time Every Time
A premium European audio brand spent eight months and twelve failed suppliers hunting for enclosures that held tolerance at volume. Rejin CNC machined their thin-wall 6063-T5 aluminum enclosure to ±0.01 mm — brushed, black-anodized and CMM-verified — then shipped 20,000+ units a month on schedule for three straight years.
See How We Solved ItGet a Free DFM Review
6063-T5Aluminum alloy, extruded + precision CNC machined
±0.01 mmTolerance held at volume, CMM verified
20,000+Enclosures per month, prototype to mass production
100%On-time delivery, 3 years running
The Story
How This Project Really Began
A real engineering story — the search, the failures, and the first DFM call that changed everything.
Every difficult CNC project starts with a problem nobody else wants to solve. This one started in Germany, where a premium audio brand was preparing to launch a new generation of control units.
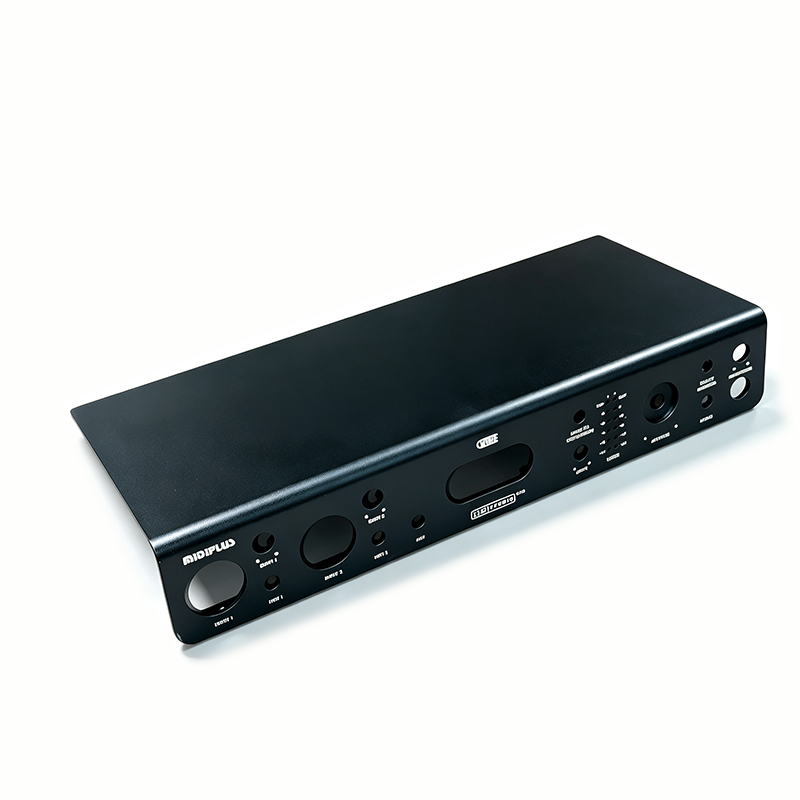
The industrial design was stunning: a slim, minimalist enclosure in brushed, black-anodized aluminum. The engineering team loved it. The manufacturing team did not. The enclosure was compact, with wall sections as thin as 1.2 mm, visible surfaces that demanded a perfectly horizontal brushed texture, and a black anodized finish that had to stay color-stable across tens of thousands of parts. On paper, it looked like a routine CNC job. In reality, it was a test that most machine shops quietly failed.
For eight months, the brand’s sourcing team searched. They evaluated machine shops in three countries, ordered sample parts from more than a dozen candidates. Some delivered accurate dimensions but rough, blotchy surfaces. Some produced a beautiful first article — and then could never repeat it at volume. One factory quoted an attractive price, quietly outsourced the anodizing to a third party, and the color drifted from batch to batch. Another could only run short runs of 500 parts, with no capacity to scale.
Samples were good. Production was not. That is the classic gap in custom CNC machining, and it was costing the brand its entire launch calendar.
“Send us your drawing, and we will tell you what is wrong with it before you spend a single dollar on tooling.”
How Rejin CNC entered the picture. The brand’s sourcing team was referred to Rejin CNC by an industry contact. Instead of quoting the drawing as-is — the way every previous supplier had done — our engineers ran a free DFM review and came back with three pages of findings: two sharp internal corners that would create stress risers and risk cracking during anodizing, an undersized thread depth on the mounting boss, and a suggested wall-thickness adjustment that would cut distortion risk in half without changing the design language. The review took 48 hours. It was delivered before any purchase order existed.
That single DFM review is what turned the conversation into a first sample order. The first article passed every single check on the customer’s list — dimension, surface, color, assembly fit. It did not just meet the standard; it set the baseline that every batch since has been measured against.
The Customer’s Pain Points
Why Previous Suppliers Could Not Deliver
Six problems, repeated across more than a dozen candidate shops.
1
Anodizing color drift
Black anodized batches drifted by ΔE > 3.0 against the master sample — unacceptable on a premium retail product where every unit must match.
2
Inconsistent brushed texture
Brushing direction and depth varied from part to part and even within the same batch, ruining the “one continuous grain” look the design required.
3
Thin-wall distortion
1.2 mm wall sections warped during machining, leaving uneven gaps at assembly and forcing costly manual rework.
4
No scale-up capability
Shops that handled 500-piece prototypes could not hold quality at 5,000, let alone 20,000+ units per month.
5
Unreliable lead times
Missed ship dates and last-minute excuses forced the brand to keep unsafe inventory buffers and risk its retail calendar.
6
No engineering feedback
Drawings were quoted as-is. Design issues surfaced only after tooling was cut and money was already spent.
Project Overview
Compact Control-Unit Enclosure for a European High-End Audio Brand
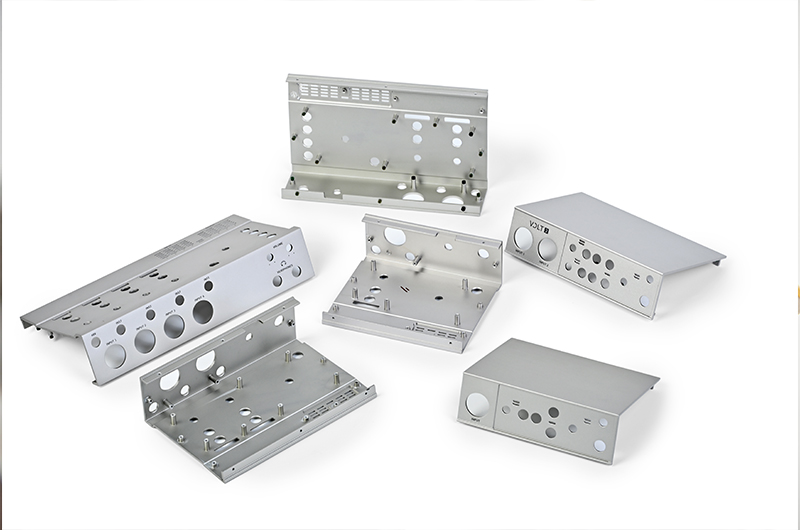
A compact control-unit enclosure for a European high-end audio brand — engineered for precision fit, a horizontal brushed texture and color-stable black anodizing, produced from a single supplier with machining, finishing, laser marking and QC all in-house.
6063-T5 extruded aluminum + CNC machining, wall thickness down to 1.2 mm
Horizontal brushed finish with color-stable black anodizing (ΔE < 1.5)
Laser-marked panels with sharp, fade-resistant graphics
Scaled from first article to 20,000+ units / month under SPC control
100% inspection on critical dimensions, every batch color-verified
Our Engineering Solution
How We Engineered the Part for Repeatable Production
The difference was never a single machine — it was a complete engineering system built around one part.
Material
6063-T5 Extruded Aluminum
Extrusion gave us a near-net inner cavity and stable material properties run after run — lower machining stock, lower cost, and far better anodizing response than die-cast blanks other shops had proposed.
Fixtures
Zero-Distortion Clamping
Custom vacuum fixtures and precision soft jaws hold every part identically without squeezing the 1.2 mm walls — the foundation of repeatable ±0.01 mm tolerance.
Process
Rough / Finish Separation
Roughing removes stock and releases internal stress; parts settle; then finishing passes hold final geometry. Toolpaths are optimized for constant chip load and minimal tool deflection.
Surface
Controlled Brushing & Anodizing
Dedicated brushing fixtures fix feed direction and pressure; anodizing bath chemistry is titrated per tank and color is verified against a retained master sample every batch.
Inspection
100% Critical-Dimension CMM
Key mounting and assembly features are measured on a CMM for every part in every batch — not sampled, not eyeballed — with data archived per production lot.
Capacity
Dedicated Cell, Planned Schedules
A dedicated machining cell and fixed monthly production windows protect this program’s lead time, so the brand can commit dates to its retail calendar with confidence.
Challenges We Overcame
Four Production Battles, and How We Won Each One
Real problems from the production floor — root cause, fix, and the result we hold today.
🧱
Thin-Wall Distortion at 1.2 mm
ProblemEarly samples warped 0.08–0.15 mm after machining — the clamp pressure and cutting heat deformed walls thinner than a credit card.
FixRedesigned fixtures to vacuum-hold from the flat reference face, split roughing from finishing, added a settling period between the two, and dropped finishing feed rates to cut heat input.
ResultFlatness held at 0.03 mm average — inside the customer’s 0.05 mm requirement — and assembly gaps became uniform across all batches.
🎯
One Continuous Brushed Grain
ProblemHand-fed brushing left visible direction changes and depth differences between parts — the “one continuous grain” look broke across a batch of 500.
FixBuilt dedicated brushing fixtures with a fixed feed path and constant pressure, and added a light-angle visual check to every inspection station.
ResultBrushed texture consistency now passes 100% of visual + light-angle checks, and the customer has approved the standard as its reference for other projects.
🎨
Color-Stable Black Anodizing
ProblemBlack anodizing drifted between batches — different dye uptake and tank age changed the black from warm to blue-ish, up to ΔE > 3.0.
FixTitrated bath chemistry before every run, standardized rack loading and current density, and verified each batch against a retained master sample with a colorimeter.
ResultBatch color now averages ΔE < 1.0 vs. master — well inside the ΔE < 1.5 requirement — and parts from different months are visually indistinguishable.
🚚
Scaling from Prototype to 20,000+ Units / Month
ProblemThe customer’s launch plan demanded a 10× volume increase in one quarter — most shops lose control of quality or lead time at that pace.
FixDedicated machining cell, parallel finishing and anodizing lines, SPC on critical dimensions, and a fixed weekly shipping schedule agreed with the customer.
Result20,000+ units per month delivered with 100% on-time shipment and zero appearance-related complaints over three years of continuous production.
Manufacturing Process
From Drawing to Finished Enclosure in 6 Controlled Steps
Every step is documented with in-process inspection, so quality is built in — not inspected in at the end.
1 DFM & Fixture Design
Engineers reviewed the CAD, optimized wall thickness and machining stock, then designed custom vacuum fixtures to hold every part identically — the foundation of repeatable tolerance.
2 CNC Machining
3-axis and 4-axis CNC milling centers rough and finish in separated operations, holding ±0.01 mm on critical features with constant chip-load toolpaths.
3 Deburring & Prep
Automated and manual deburring removes edge marks, then parts are cleaned and prepped so the brushed texture comes out flawless.
4 Brushing & Black Anodizing
Horizontal brushing gives the signature grain; sulfuric anodizing in a titrated bath produces a color-stable black, verified against the master sample.
5 Laser Marking
Logos, model numbers and regulatory marks are laser-marked with fixture-located precision for sharp, fade-resistant graphics.
6 100% Inspection & Packing
Every part is CMM-checked on critical dimensions, color-verified and individually wrapped to prevent scratches before export packaging.
Quality Assurance
Measured Results, Not Promises
Every key specification is verified with CMM, profilometer and color measurement on every production batch — data archived per lot for full traceability.
Specification
Requirement
Achieved
Method
Machining tolerance
±0.01 mm
±0.01 mm
CMM measurement
Surface flatness
0.05 mm max
0.03 mm avg
Height gauge / granite plate
Anodizing color (black)
ΔE < 1.5 vs. master
ΔE < 1.0 avg
Colorimeter
Brushed texture
Consistent grain direction
100% pass
Visual + light-angle inspection
Salt spray resistance
72 h, no corrosion
Passed
ASTM B117
Laser mark durability
No fade after use
Passed
Abrasion / solvent test
Why Rejin CNC
What Makes Us Different From a Commodity Machine Shop
The brand compared us against shops in three countries. Here is what closed the deal.
vs. quote-as-is shops
DFM before the order
We review the drawing and flag manufacturability issues before you spend on tooling — the review that first won this customer is free and standard for every project.
vs. outsourced finishing
Finishing 100% in-house
Brushing, anodizing and laser marking run under our own roof — no hand-offs, no color drift, no third-party excuses between machining and the finished part.
vs. batch sampling
100% inspection, not AQL sampling
Critical dimensions are CMM-measured on every part and color is verified every batch, so a defect never ships to your line.
vs. sales-led support
Engineers answer your questions
You talk directly to the people who run the machines and the process — technical answers in hours, not sales promises in weeks.
Project Results
What Three Years of Partnership Delivered
The first batch fully met the brand’s retail standards, and the relationship has only grown since.
0Appearance-related complaints from end users
100%On-time monthly deliveries, zero delays
+20%Customer repurchase rate after metal upgrade
3Years of continuous production partnership
Customer Feedback
What the OEM Buyers Say
Direct quotes from the people who run this program on the customer side.
“We spent eight months looking for a partner who could hold both tolerance and surface finish at volume. Rejin’s first article passed everything — we stopped looking that day.”
Purchasing DirectorEuropean Electronics Brand
“The brushed texture and black anodizing are identical to our reference sample even after three years of production. Color has never been a discussion point on a single batch.”
Quality ManagerEuropean Audio Brand
“The metal material has an outstanding tactile feel. Customer repurchase rates increased by 20%, making them a key partner in our product upgrades.”
Product ManagerNorth American Audio Equipment Supplier
Free DFM Check · Quote in 24 Hours
Have a Similar CNC Enclosure or Audio Part Project?
Send us your CAD and get a free DFM check with a detailed quotation within 24 hours.
Get a Quote in 24 Hours →Explore CNC Capabilities
(function(){function m(){var w=document.querySelector(".rjc-wrap"),h=document.querySelector(".rjc-hero"),b=document.querySelector(".breadcrumb-my"),s=document.querySelector(".service-details-content");if(!w||!h||!b||!s)return;var t=s.querySelector("h1");if(h.nextElementSibling!==b){w.insertBefore(b,h.nextElementSibling);}if(t&&b.nextElementSibling!==t){w.insertBefore(t,b.nextElementSibling);}}if(document.readyState==="loading"){document.addEventListener("DOMContentLoaded",m);}else{m();}})();